Formula details
Product Details
Overview
Continuous Annealing Working Principle and Processing Scope
As a specialized OEM continuous annealing furnace factory, we engineer automated thermal processing systems built for continuous, high-volume production lines. Our furnaces advance workpieces seamlessly through dedicated, sealed chambers to complete exact metallurgical cycles without atmospheric exposure or surface oxidation.
[Charge Vestibule] ➔ [Controlled Heating] ➔ [Isothermal Soaking] ➔ [Controlled Rapid/Slow Cooling] ➔ [Discharge]
│ │ │ │
└────────────── Continuous Protective Atmosphere (N2 / H2 / Cracked NH3) ─────────┘
Controlled Heating, Soaking, and Cooling Cycles
Our engineering team configures every thermal profile to meet specific mechanical property requirements, eliminating grain growth defects and surface discoloration:
-
- Multi-Zone Preheating & Heating: Progressive heating ramps eliminate thermal shock and prevent component distortion.
- Precision Isothermal Soaking: Closed-loop PID controls hold soak zones within tight tolerances to achieve homogeneous phase transformation.
- Engineered Cooling Options: Systems include slow-cooling jackets for grain refinement or high-convective gas-quenching zones for rapid cooling cycles.
Comprehensive Heat Treatment Capabilities
As a dedicated OEM continuous annealing furnace exporter, we design our equipment to execute diverse heat-treating cycles within a single continuous footprint:
-
- Bright Annealing: Finished surfaces emerge clean, mirror-bright, and scale-free under protective atmospheres, eliminating secondary pickling operations.
- Stress Relief: Relieves residual stresses induced by heavy cold drawing, stamping, roll forming, or machining.
- Recrystallization Annealing: Restores ductility in cold-worked alloys to permit severe subsequent deep-drawing or bending steps.
- Normalizing: Refines coarse dendritic structures in forgings and structural raw stock to ensure uniform grain size and hardness.
Alloy Processing Compatibility
| Material Category | Primary Processing Alloys | Typical Thermal Range | Protective Atmosphere | Processing Result |
|---|---|---|---|---|
| Stainless Steel | Austenitic (300 series), Ferritic (400 series) | 1,010°C – 1,150°C | Pure H2 or Cracked Ammonia | Scale-free bright finish; complete carbide dissolution |
| Carbon & Alloy Steel | Low/medium carbon steels, spring steels | 680°C – 920°C | N2 + H2 blend / Endo gas | Uniform microstructures; scale-free stress relief |
| Copper & Brass | OFC copper, cartridge brass, bronze alloys | 450°C – 700°C | Nitrogen-rich blend | High electrical conductivity; zero surface tarnish |
| Aluminum Alloys | 3000, 5000, and 6000 series stock | 350°C – 520°C | Dry Nitrogen / Inert Air | Consistent yield strength; full ductility recovery |
OEM Continuous Annealing Furnace Conveyance and Hearth Configurations
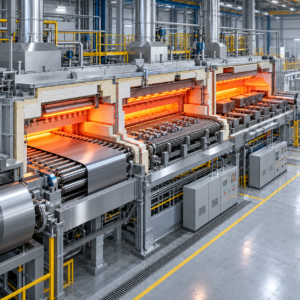
Conveyance determines production reliability; an undersized drive or incorrect hearth design causes distortion, jamming, and uneven thermal exposure. We engineer four primary transport configurations to meet diverse industrial volumes.
Continuous Mesh Belt Conveyors for Small Stampings and Fasteners
Our mesh belt continuous furnace lines process high-volume, small-to-medium parts without part-to-part impingement.
Belt Materials: Woven high-nickel alloys (SUS314, SUS310S, or Inconel) resistant to thermal fatigue and stretch under load.
Drive Systems: Variable frequency AC drives paired with pneumatic tensioning and auto-tracking mechanisms to prevent belt slippage and edge fraying.
Parts Handled: Stamped automotive brackets, deep-drawn shells, self-tapping screws, rivets, and chain links.
Heavy-Duty Roller Hearth Systems for Pipes, Bars, and Plates
For long structural stock and high-tonnage throughput, our roller hearth annealing furnace systems deliver continuous linear movement without carrier distortion. Understanding key roller hearth furnace advantages for efficient heating allows our engineering team to design custom roller profiles for your exact load specs.
Roll Construction: Centrifugally cast heat-resistant alloy rollers inside the hot zone, transitioned to water-cooled alloy rollers in rapid cooling sections.
Drive Mechanism: External chain-and-sprocket or bevel gear line-shaft drives, isolated from chamber heat to minimize bearing wear.
Parts Handled: Seamless stainless steel tubes, copper tubing bundles, solid steel bars, and heavy plates.
Pusher and Walking Beam Mechanisms for High-Load Structural Forgings
When batch trays carry extremely dense, heavy structural forgings, mechanical drive belts are impractical. Our oem continuous annealing furnace exporter division manufactures heavy-duty walking beam and hydraulic pusher hearths:
Positive Step Indexing: Hydraulically driven beams lift, advance, set down, and return work trays through discrete temperature zones.
Zero Hearth Drag: Walking beam designs eliminate hearth plate friction, extending alloy tray life and preventing mechanical shock to hot components.
Parts Handled: Automotive crankshafts, heavy bearing rings, transmission gear blanks, and heavy forged flanges.
Strand and Multi-Line Systems for Continuous Wire and Strip Processing
For linear mills requiring high-speed bright annealing, our multi-strand continuous lines deliver exact tension and atmosphere control.
Multi-Tube Muffling: Individual alloy muffle tubes running through the heating zone maintain high-purity hydrogen atmospheres with minimal gas consumption.
Tension Control: Closed-loop payoff and take-up capstans maintain stable line tension, preventing strip necking or wire elongation at peak temperatures.
Parts Handled: Stainless steel strip, high-carbon spring wire, copper electrical strands, and nickel alloy foil.
OEM Continuous Annealing Furnace Heating & Atmosphere Control
Heating System Configurations: Electric and Gas
We offer both electric resistance systems and high-efficiency gas combustion designs:
-
- Electric Resistance Elements: We install heavy-gauge Fe-Cr-Al (Kanthal) or silicon carbide (SiC) elements distributed across independent heating zones. Backed by multi-layer, low-thermal-mass ceramic fiber insulation modules, these systems minimize exterior shell heat loss, shorten heat-up times, and reduce idle power draw.
- Indirect Radiant Tube Burners: For facilities running natural gas or LPG, our oem continuous annealing furnace exporter division builds continuous lines equipped with alloy radiant tubes (SUS310S or centrifugal-cast alloy) paired with integrated recuperative burners. These recuperators capture exhaust heat to preheat combustion air up to 450°C, cutting fuel consumption by 20% to 30%.
- Direct Gas-Fired Options: Available for open-atmosphere normalizing or preheating zones where oxide-free finishes are mechanically pickled downstream.
| Parameter | Electric Resistance Heating | Indirect Gas Radiant Tubes |
|---|---|---|
| Max Operating Temp | Up to 1150°C | Up to 1050°C |
| Thermal Uniformity | ±3°C to ±5°C across the belt/hearth | ±5°C across all active zones |
| Combustion Efficiency | ~95% electrical-to-thermal transfer | >75% with self-recuperative burners |
| Typical Application | Precision wire, strip, stainless & copper | Carbon steel tubes, forgings, structural bar |
Multi-Zone Thermal Profiling & Soaking Control
Every furnace chamber features multi-zone PID loops driven by industrial PLC automation. By tuning individual preheat, ramp, soaking, and slow-cool sections, our lines prevent thermal shock in heavy cross-sections and eliminate grain size variance. Multi-point Type K, N, or S thermocouples monitor both atmosphere temperature and muffle wall temperatures to enforce accurate soak cycles.
Protective Atmosphere Management & Dew-Point Control
To guarantee scale-free, mirror-bright surface finishes, our factory integrates proven atmosphere skids engineered for pure gases or blended chemistries:
-
- Atmosphere Types: We supply fully integrated piping skids for cracked ammonia (75% H_2 / 25% N_2), pre-blended bulk nitrogen-hydrogen mixes (95/5 to 75/25), and 100% pure hydrogen. For demanding alloy cycles requiring dry, highly reducing environments, our continuous systems draw on the gas delivery and safety dynamics proven in our hydrogen atmosphere furnace high-temperature heating equipment.
- Real-Time Dew-Point Monitoring: In-line ceramic or chilled-mirror moisture analyzers continuously track dew points inside the hot zone and cooling tunnels, maintaining working thresholds between -40°C and -65°C.
- Gas Curtains and Physical Seals: Both charge and discharge vestibules use nitrogen barrier curtains, adjustable physical baffles, and automatic exhaust burn-off torches. This prevents oxygen ingress, stops volatile oil vapors from entering the hot muffle, and keeps flammable process gases below explosive ambient thresholds.
OEM Continuous Annealing Furnace Factory Technical Parameters
Core Engineering Specifications and Capacity Sizing
Every continuous line leaves our plant pre-commissioned to deliver tight soak profiles and low energy loss per metric ton of processed metal:
-
- Operating Temperatures: Rated continuously from 650°C to 1150°C (1202°F to 2102°F) depending on alloy metallurgy (carbon steel, 300/400-series stainless, brass, or copper).
- Thermal Uniformity: ±3°C to ±5°C across the effective hearth cross-section, verified via calibrated multi-point thermocouple trailing wire surveys.
- Production Throughput: Scalable from 100 kg/h for fine precision stampings up to 3,500 kg/h for continuous tube, wire, and structural coil processing.
- Conveyance Speed Range: Variable frequency drives (VFD) provide smooth stepless belt or roller speeds ranging from 50 mm/min to 1,200 mm/min, optimizing dwell time inside the heating zone.
- Hearth & Chamber Dimensions: Usable belt or roller widths from 300 mm to 1,500 mm; total system lengths span from 12 meters to over 45 meters, encompassing preheat, multi-zone soaking, jacketed water cooling, and convective fast-cool tunnels.
When evaluating plant capital layout against batch setups, comparing total energy load via our vacuum furnace cost and price guide by capacity helps determine whether continuous or batch conveyance yields the best utility return for your target volume.
Baseline Utility and Atmosphere Consumption Matrix
Our standard engineering builds balance gas tight atmosphere retention with minimized utility consumption across all heating modes:
| Parameter | Mesh Belt Model (Small Parts) | Roller Hearth Model (Tubes & Bars) | Strand / Wire Model (Multi-Line) |
|---|---|---|---|
| Max Working Temp | 1,120°C (2,048°F) | 1,150°C (2,102°F) | 1,180°C (2,156°F) |
| Heating Method | Electric (NiCr/FeCrAl) or Gas Radiant Tubes | Recuperative Gas Radiant Tubes | High-Power Electric Ceramic Elements |
| Atmosphere Gas | N₂ + H₂ blend / Cracked Ammonia | Pure Nitrogen / Exothermic Gas | High-purity H₂ (up to 100%) |
| Atmosphere Flow Rate | 15 – 45 Nm³/h | 50 – 120 Nm³/h | 10 – 30 Nm³/h |
| Cooling Water Flow | 8 – 15 m³/h (Closed Loop) | 20 – 40 m³/h (Closed Loop) | 5 – 12 m³/h (Chilled Loop) |
| Typical Connected Load | 90 kW – 350 kW | 250 kW – 850 kW | 75 kW – 220 kW |
As a global OEM continuous annealing furnace exporter, we customize these primary parameters to match regional factory voltage, gas pressure supplies, and protective atmosphere systems prior to factory assembly.
Structural Build and Proprietary Engineering Features
High-Density Ceramic Fiber Lining
To minimize exterior heat loss and stabilize interior zone temperatures, our engineering team uses a multi-layer insulation profile:
-
- Refractory Layering: We combine high-purity ceramic fiber modules (128 kg/m³ to 160 kg/m³) with microporous backup boards. This structural insulation matches the heavy-duty thermal standards applied across our industrial heating equipment, including specialized designs like our high-temperature roller kiln for advanced ceramics.
- Low Skin Temperatures: Outer furnace shell temperatures stay under 45°C above ambient during continuous 1,150°C operation, directly lowering utility draw.
- Engineered Anchoring: Heat-resistant alloy studs secure the modules in a parquet arrangement to prevent shrinkage cracks and eliminate thermal bypass paths.
Creep-Resistant SUS310S and Inconel Muffles
For processes requiring sealed protective atmospheres, we build our muffles in-house using heavy-gauge nickel-chromium alloys:
-
- Material Selection: Standard builds feature 8 mm to 12 mm thick SUS310S for operations up to 1,050°C, and Inconel 600 or 601 for aggressive thermal duties up to 1,180°C.
- Corrugated Geometry: Continuous sidewall corrugation allows natural thermal expansion and contraction without localized stress points, drastically extending muffle service life under hydrogen atmospheres.
- Atmosphere Sealing: Flanged expansion joints with water-cooled elastomer gaskets maintain atmosphere purity and hold working pressure without leakage.
Precision Cooling Configurations
Controlled metallurgical cooling prevents oxidation and sets target hardness levels right before discharge:
-
- Dual-Chamber Water Jackets: Fabricated with corrosion-resistant 304 stainless steel inner walls, our cooling jackets provide uniform temperature drop rates through counter-flow cooling water loops.
- Jet-Gas Recirculation: For high-throughput bright annealing lines, we integrate enclosed high-velocity gas cooling zones. Variable-frequency blowers direct cooled protective atmosphere directly onto the workpieces via directional jet nozzles, speeding up cycle times while preventing surface tarnishing.
| Assembly Subsystem | Standard Factory Specification | Production Advantage |
|---|---|---|
| Furnace Shell | 6 mm–10 mm Q235B plate, reinforced structural steel | Zero flex under load; gas-tight continuous perimeter welds |
| Hot Zone Muffle | SUS310S / Inconel 601 (8–12 mm thickness) | High creep resistance and thermal shock durability |
| Thermal Insulation | 128–160 kg/m³ ceramic fiber + calcium silicate backup | Up to 28% reduced idle energy consumption |
| Cooling Section | Multi-stage water jacket or protective gas jet cooler | Uniform grain formation; clean, oxidation-free discharge |
| Control Architecture | Siemens S7-1500 / Mitsubishi PLC with 15-inch HMI | Automated recipe tracking, event logging, and remote diagnostics |
Industrial PLC Automation and SCADA Data Logging
As a dedicated OEM continuous annealing furnace exporter, we equip every processing line with complete digital management controls:
-
- Integrated Multi-Recipe Control: Operators switch between material grades via pre-programmed cycle recipes that automate zone temperatures, drive speeds, and atmosphere flow rates.
- Comprehensive Data Tracking: The SCADA architecture captures continuous heating curves, dew-point values, and motor loads to CSV/SQL databases for full automotive and aerospace lot traceability.
- Safety Interlocks: Independent over-temperature controllers, water flow monitors, atmosphere purge interlocks, and emergency stop circuits run through redundant hardwired fail-safes.
OEM Continuous Annealing Furnace Factory Production and Quality Control
As an experienced OEM continuous annealing furnace factory, we control every manufacturing phase under one roof. We do not outsource critical structural or thermal fabrication. By keeping heavy metalworking, machining, assembly, and testing inside our facility, our engineering team guarantees tight dimensional tolerances, gas-tight chamber integrity, and long service life for every continuous line we ship.
In-House Heavy Metal Fabrication
Every furnace frame begins with structural steel processing in our main fabrication bay:
CNC Laser and Plasma Cutting: High-definition cutting of structural plate up to 30 mm thick ensures clean fit-up for all casing joints.
Plate Rolling and Section Forming: Heavy roll-forming machines shape shell segments, transition hoods, and water jackets with zero seam distortion.
Automatic Submerged Arc Welding (SAW): Structural framework and outer shell seams receive automated continuous welds to guarantee air-tight sealing against protective gas leaks.
Raw Material Inspection ──> CNC Profile Cutting ──> Precision Machining ──> Submerged Arc Welding ──> NDT & FAT Testing
Precision Machining of Conveyance Drives
Conveyance reliability determines uptime. In our CNC machining center, we turn and balance drive shafts, sprockets, and transport rolls to prevent line jams and uneven belt tracking:
Drive Shafts and Rollers: Turned on heavy-duty CNC lathes to runout tolerances within ±0.02 mm. This is critical for our heavy-duty roller hearth furnace lines and high-speed multi-tube conveyors.
Drive Spockets and Drum Assemblies: Precision-milled to preserve belt geometry and eliminate wear points across continuous mesh belt annealing furnace systems.
Dynamic Balancing: Every drive drum and high-temperature recirculation fan wheel undergoes dynamic balancing to ISO 1940 Grade G2.5 to eliminate vibration at operating temperatures.
Weld Inspection and Sensor Calibration
Before any equipment moves to electrical assembly, our QC team executes strict non-destructive testing (NDT) and instrumentation verification:
| Inspection Phase | Method / Standard | Acceptance Criteria |
|---|---|---|
| Muffle & Casing Seams | Dye Penetrant (PT) & Ultrasonic Testing (UT) | Zero micro-cracks, complete penetration on alloy welds |
| Atmosphere Enclosures | Helium leak testing & positive pressure hold | Pressure decay rate < 50 Pa/hr at 1.5x working pressure |
| Thermal Profiling | 9-point to 12-point secondary thermocouple array | Uniformity class verified to AMS 2750 standard |
| Cooling Jackets | Hydrostatic pressure testing at 0.6 MPa | Zero pressure drop and zero seam sweating over 4 hours |
Factory Acceptance Testing (FAT)
Every custom line undergoes a full dry-run FAT on our factory floor before tear-down for shipment:
Mechanical Dry Runs: Continuous 24- to 48-hour mechanical operation to test motor amperage draws, belt tracking, drive chain tension, and bearing temperatures.
Wiring and SCADA Diagnostics: End-to-end I/O check of the PLC cabinet, emergency stops, safety interlocks, burner management controllers, and gas flow sensors.
Gas Train Pressure Hold: Piping networks for nitrogen, hydrogen, or cracked ammonia undergo full static pressure checks to confirm zero leakage before clearance for global dispatch.
OEM Continuous Annealing Furnace Exporter: Logistics and Global Field Support
As a premier oem continuous annealing furnace factory, our delivery responsibility extends well beyond our workshop floor. Delivering high-tonnage thermal lines across international borders requires reliable protective packaging, standard container design, and dependable on-site engineering support. We treat equipment logistics with the exact same engineering precision we apply to temperature uniformity and atmosphere controls.
Seaworthy Packing and Anti-Corrosion Protection
Long ocean transits expose machinery to salt spray, humidity swings, and physical impacts. To guarantee zero damage or surface oxidation upon arrival, our packing department executes a multi-barrier export protocol:
Vacuum Barrier Enclosures: Critical heating chambers, alloy muffles, drive motors, and electrical cabinets are sealed inside heavy-gauge aluminum-plastic vacuum foil with industrial desiccants.
Corrosion Inhibitors: All bare metal surfaces, drive shafts, and conveyance rollers receive a multi-layer VCI (Vapor Corrosion Inhibitor) application.
Reinforced Casing: Structural sub-assemblies are secured within heavy-duty, fumigated solid timber cases lined with waterproof damp-proof membranes, meeting global ISPM-15 standards.
Modular Skid Architecture for Global Shipping
Designing continuous furnaces for sea freight demands smart modular engineering. Our oem continuous annealing furnace exporter division builds each production line on independent, high-rigidity structural skids. This architecture avoids costly, complex logistics:
Container Compatibility: Standard modules fit cleanly inside 40ft HQ dry containers, cutting ocean freight overhead substantially.
Outsized Modules: Extra-wide cooling tunnels, large radiant canopies, and wide roller hearths travel on pre-braced Flat Rack containers with certified lifting lugs for fast port handling.
Plug-and-Produce Piping: Atmosphere manifolds, electrical cable trays, and water cooling lines feature quick-disconnect modular interfaces, cutting on-site mechanical alignment down to a few days. Much like our transport-ready vacuum annealing furnace systems, every interface is match-marked at the factory before packing.
| Shipment Section | Transport Method | Packaging Standard | Safeguard Features |
|---|---|---|---|
| Heating & Muffle Zones | 40ft HQ / Flat Rack | Vacuum foil + Timber framing | Multi-point tie-downs & moisture barrier |
| Cooling & Drive Beds | 40ft HQ Container | VCI wrap + Steel skid bolting | Anti-vibration blocks & desiccant packs |
| HMI & PLC Control Cabinets | 20ft / 40ft Standard | Double-wall wooden export crates | Shock sensors & climate-sealed barrier |
| Piping & Auxiliary Spares | 40ft HQ Container | Steel-strapped internal crates | Component-matched tagging & inventory list |
International Compliance and Field Commissioning
We eliminate customs delays and compliance headaches by bundling certified documentation packages with every shipment. Every export project includes full CE conformity certificates, ISO 9001 factory documentation, mechanical mill test reports for all high-temperature alloys, and clear schematic wiring layouts.
Once equipment arrives at your facility, our international field technicians handle deployment from start to finish:
Turnkey Mechanical Installation: Leveling, modular structural anchoring, drive line alignment, and utility hookups.
Atmosphere and Thermal Dry-Runs: Helium leak checks, protective gas purge verifications, and AMS 2750 multi-zone heat profiling.
Operator and Maintenance Training: Hands-on instruction covering recipe setup, SCADA operation, seal replacements, and preventive safety protocols for plant maintenance crews.
Industrial Manufacturing Applications
As an established OEM continuous annealing furnace factory, we build thermal processing lines tailored to high-volume manufacturing sectors where surface finish, ductility, and structural uniformity cannot be compromised. Our systems integrate cleanly into existing production workflows, providing consistent results across a wide range of industrial heat treatment tasks.
Automotive Fuel Rails, Brake Lines, and Deep-Drawn Parts
Automotive components require zero oxidation and exceptional fatigue resistance. Our continuous lines handle:
Precision tubing: Seamless and welded stainless steel fuel rails, direct injection systems, and hydraulic brake lines.
Deep-drawn stampings: Oil filter housings, transmission clutch shells, and airbag canisters that require inter-stage stress relief annealing to restore formability without pickling.
Consistent metallurgy: Tight temperature uniformity eliminates work hardening across localized draw zones.
Hardware Fasteners, Screws, Chains, and Rivets
For hardware producers handling bulk throughput, our mesh belt furnace systems deliver reliable continuous processing:
High-tensile fasteners: Relieving stresses in cold-headed screws, aerospace-grade rivets, and heavy-duty industrial chains.
Decarburization-free surfaces: Controlled protective gas chemistry prevents surface carbon loss, protecting thread integrity and strength ratings.
Bulk handling: Continuous, smooth feeding avoids part tangling, nicking, or uneven thermal exposure.
Continuous Bright Annealing for Stainless Steel Tubes and Copper Coils
Operating as a dedicated OEM continuous annealing furnace exporter, we design heavy-duty roller hearth and muffle lines specifically for high-capacity mill environments:
Stainless steel tubes (300/400 series): Rapid cooling prevents carbide precipitation, yielding corrosion-resistant, mirror-bright outer and inner surfaces.
Copper tubing and pancake coils: Low dew-point protective atmospheres guarantee bright, residue-free copper tubes ready for HVAC and refrigeration installations.
Straight lengths and coils: Modular conveyance setups accommodate both long straight lengths and basket-loaded coiled tubing.
Precision Electronics, Lead Frames, and Magnetic Shielding
Our specialized atmospheres accommodate high-tech sectors demanding extremely pure processing zones:
Semiconductor lead frames: Copper-iron and nickel-iron strip alloys treated with zero discoloration for dependable downstream plating and wire bonding.
Soft magnetic alloys: Permalloy, silicon steel, and Mu-Metal annealed for maximum magnetic permeability and minimum coercive force.
Ultra-thin metal foils: Tension-controlled strand feeds eliminate buckling, stretching, or thermal shock during high-speed continuous runs.
OEM Continuous Annealing Furnace Sourcing FAQs
How do we maintain low dew points to prevent metal oxidation?
We build tight atmosphere seals directly into our process tunnels to achieve dew points as low as -40°C to -60°C:
-
- Atmosphere curtains: Flame curtains and nitrogen gas purge barriers at entry and exit vestibules eliminate ambient oxygen ingress.
- Hermetic muffle design: Fully welded, continuous alloy muffles keep protective process gas separate from insulation and heating elements.
- Positive pressure balance: Automatic differential pressure regulators continuously maintain a slight positive furnace pressure to stop air leaks.
- Real-time sensing: Built-in ceramic dew-point sensors and oxygen analyzers link directly to the PLC to trigger gas-flow adjustments automatically.
What is our factory manufacturing lead time for custom continuous lines?
As an established oem continuous annealing furnace exporter, our lead times depend on system size, hearth mechanism, and automation scope:
| Equipment Scope | Engineering & Design | Fabrication & Assembly | FAT & Testing | Total Lead Time |
|---|---|---|---|---|
| Standard Mesh Belt Line | 2–3 weeks | 6–8 weeks | 1–2 weeks | 10–12 weeks |
| Roller Hearth Annealing Line | 3–4 weeks | 8–12 weeks | 2 weeks | 14–18 weeks |
| Fully Customized Turnkey Setup | 4–6 weeks | 12–16 weeks | 2–3 weeks | 18–24 weeks |
Can we integrate this furnace into your existing stamping or drawing setup?
Yes. We configure our continuous equipment to align with both upstream stamping presses and downstream finishing equipment:
-
- Synchronized conveyors: Variable frequency drives and encoder-based pacing tie furnace conveyor speeds to your press output or spooling lines.
- Automated material handling: We supply turn-key feed hoppers, vibratory orienters, wash systems, and pick-and-place gantry loaders.
- Control interoperability: Our PLC architectures use standard industrial protocols (Profinet, Ethernet/IP, Modbus) to communicate directly with your plant-wide MES or SCADA system.
- For stamping plants processing stamped hardware or cold-headed fasteners, our custom mesh belt continuous furnace configurations integrate smoothly with in-line degreasers and automated bins.
What are the utility requirements for electricity, gas, and cooling water?
Utility demands vary with thermal throughput, heating method, and atmosphere selection:
-
- Electrical supply: 3-phase 380V/440V/480V, 50/60 Hz. Connected power ranges from 45 kW for compact units up to 600+ kW for heavy production lines.
- Protective process atmosphere: Pure nitrogen (99.999%), hydrogen blends, or dissociated ammonia supply delivered at 0.2–0.4 MPa.
- Cooling water: Closed-loop industrial cooling loop with inlet water temperatures below 32°C, supply pressure of 0.2–0.3 MPa, and filtration to prevent scaling inside water jackets.
- Burner fuel (if gas-fired): Natural gas or LPG at stable delivery pressure (typical 20–50 kPa regulated supply).
How do we supply and ship replacement wear parts internationally?
Our factory maintains complete lifecycle support for all exported machinery:
-
- Commissioning spare kits: Every export shipment includes a 2-year operational wear pack containing spare thermocouples, drive belts, heating elements, and gaskets.
- Standardized international components: We use internationally recognized brands (Siemens, Schneider, Omron, Eurotherm) so field technicians can source local electrical components easily.
- Fast-track mechanical parts: Critical custom mechanical spares—including drive sprockets, hearth rollers, and woven mesh sections—ship via DHL or air freight within 48 to 72 hours of request.