Vacuum Furnace Working Principle & Chamber System Anatomy
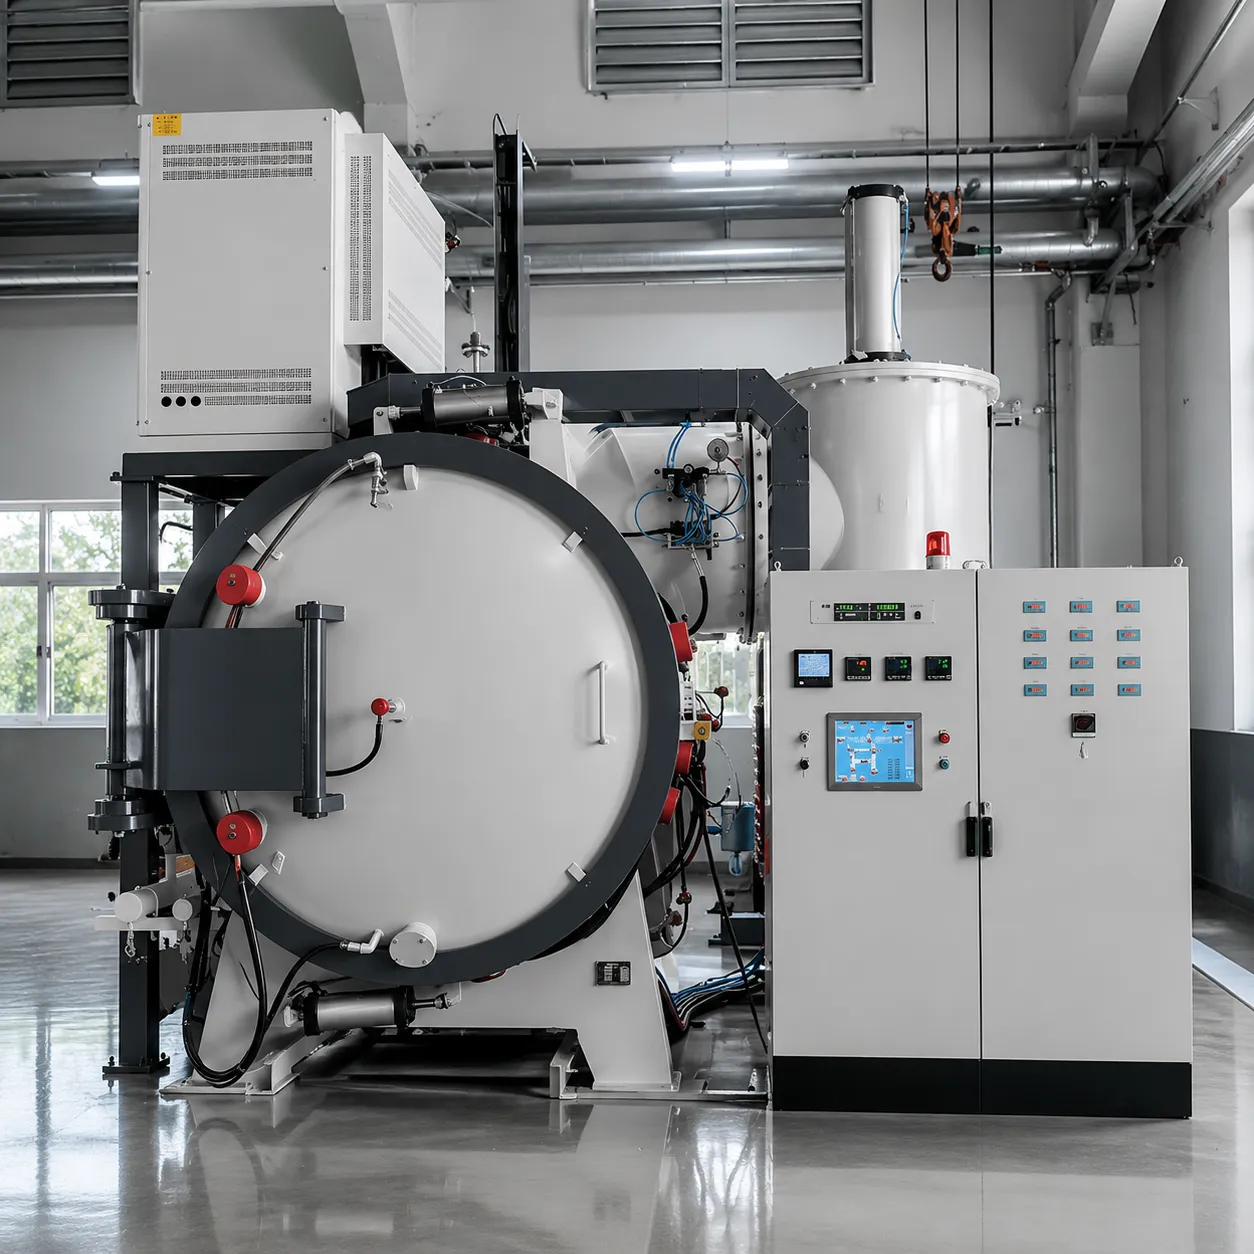
High-vacuum thermal processing fundamentally transforms industrial metallurgy by removing reactive gas species prior to thermal exposure. Haitem Furnace engineers advanced vacuum furnaces and heat treatment systems operating across ultra-clean pressure regimes from 10⁻¹ Pa down to 10⁻⁵ Pa, ensuring pristine surface metallurgy, zero oxidation, zero decarburization, and precise microstructural evolution for critical industrial applications.
Thermodynamics of High-Vacuum Environments (10⁻¹ Pa to 10⁻⁵ Pa)
At ambient atmospheric pressure, elevated heat processing causes rapid oxidation, surface scaling, and irreversible carbon depletion across high-performance alloys. Operating within a high-vacuum regime fundamentally alters gas-metal kinetics by evacuating atmospheric oxygen, water vapor, and residual hydrocarbons before heating begins.
In evacuated chambers operating between 10⁻¹ Pa and 10⁻⁵ Pa, the partial pressure of reactive oxygen drops far below the thermodynamic oxidation equilibrium line for sensitive materials like titanium, superalloys, refractory metals, and high-speed tool steels. This controlled thermal processing environment delivers three critical metallurgical advantages during every cycle:
Complete Oxidation Elimination
Evacuated chamber conditions eliminate atmospheric oxygen molecules. Engineered components emerge with bright, unblemished surfaces, eliminating post-process acid pickling, bead blasting, or costly secondary grinding.
Precision Decarburization Control
By strictly controlling residual gas partial pressures, tool steels and high-carbon alloys retain critical surface carbon content. Hardness gradients remain uniform from core to case without surface depletion.
Deep Alloy Vacuum Degassing
Extremely low partial pressures draw out entrapped volatile gases—such as hydrogen, nitrogen, and oxygen—from the metal matrix during heating, preventing hydrogen embrittlement and enhancing fatigue limit performance.
Hot Zone Architecture: All-Metallic vs. Graphite & C-C Composites
Selecting the ideal vacuum furnace hot zone requires balancing maximum operational temperatures, work material chemistry, vacuum level requirements, and thermal efficiency. Both metallic molybdenum/tungsten and graphite composite heating elements offer unique metallurgical advantages for specialized heat treatment cycles.
All-Metallic (Molybdenum / Tungsten) Hot Zone Configuration
Engineered with multi-layer molybdenum or tungsten radiation shields and matching metallic heating elements, all-metallic hot zones create an ultra-clean, dust-free thermal environment. This configuration guarantees absolute protection against carbon contamination during critical vacuum thermal processing.
- Max Continuous Temp: Up to 1350°C (Molybdenum) / 2400°C (Tungsten)
- Carbon Pickup Risk: Absolute Zero (Essential for titanium & medical implants)
- Outgassing Rate: Exceptionally low outgassing for rapid pump-down cycles
- Atmosphere Compatibility: High vacuum, Argon, Nitrogen, Hydrogen, and inert gases
Primary Industrial Applications
Crucial for aerospace superalloys, medical titanium implants, nuclear component brazing, electronic tube manufacturing, and high-purity single-crystal growth where even micro-ppm carbon absorption causes grain boundary weakening.
| Performance Metric | All-Metallic (Molybdenum / Tungsten) | Graphite & C-C Composites |
|---|---|---|
| Ultimate Vacuum Capability | Down to 10⁻⁵ Pa (10⁻⁷ mbar) ultra-high vacuum | Typically 10⁻³ Pa to 10⁻⁴ Pa high vacuum |
| Temperature Uniformity | ±3°C to ±5°C via multi-zone independent control | ±5°C across the full working hot zone volume |
| Heating Element Lifespan | Extremely long in clean vacuum; sensitive to oxygen exposure | Exceptional structural longevity under rapid thermal cycling |
| Power Consumption Efficiency | Moderate radiation heat loss at extreme temperatures | Superior thermal insulation efficiency; reduced power consumption |
Vacuum Pumping System Engineering Logic
Achieving rapid evacuations and maintaining reliable vacuum levels under heavy gas outgassing requires precise sizing of primary backing pumps and high-vacuum boosters. Haitem customizes multi-stage vacuum pump trains based on furnace volume, target vacuum pressure, and process gas loading.
Primary Backing Stage (Atmosphere to 10 Pa)
The primary backing stage provides roughing capability, evacuating the furnace chamber from ambient atmospheric pressure down to intermediate crossover pressures. Pump selection defines maintenance frequency and fluid exposure:
- Rotary Vane Pumps: Reliable, oil-sealed positive displacement pumps engineered for standard industrial heat treatment operations.
- Dry Screw Pumps: Fully oil-free mechanical backing systems that eliminate hydrocarbon backstreaming into sensitive vacuum chambers.
- Roots Blowers: High-displacement mechanical boosters paired with primary pumps to accelerate volumetric evacuation speed by 5x to 10x.
High-Vacuum Booster Stage (10 Pa to 10⁻⁵ Pa)
When chamber pressure reaches the crossover setpoint, high-vacuum booster pumps initiate to achieve deep vacuum processing regimes required for critical metallurgy:
- Oil Diffusion Pumps: High-speed vapor jet pumps offering exceptional volumetric throughput for heavy industrial vacuum processing at economical costs.
- Turbomolecular Pumps (TMP): High-speed kinetic momentum pumps generating completely oil-free, high-purity ultra-vacuum processing conditions.
- Automated Crossover Valves: Electro-pneumatic safety valves dynamically isolate booster systems to prevent backstreaming during high-pressure cycles.
High-Pressure Gas Quenching (HPGQ) Dynamics (2 bar to 15 bar)
Controlled, rapid cooling inside the vacuum chamber enables precise martensitic phase transformation while minimizing thermal gradients and part distortion. Haitem high-pressure gas quenching technology utilizes directional gas management to achieve repeatable transformation metallurgy.
Pressure & Cooling Rates
Gas quenching pressures adjustable from 2 bar up to 15 bar absolute deliver cooling velocities matching traditional oil quenching, while maintaining bright, clean part surfaces without oil disposal or washing steps.
Directional Nozzle Arrays
360-degree radial nozzle arrangements with alternating top-to-bottom and side-to-side gas flow paths direct high-velocity coolant through dense workloads, preventing thermal distortion and non-uniform core cooling.
Inert Quench Gas Selection
Configurable for Nitrogen (N₂), Argon (Ar), or Helium (He). High-density Helium gas quenching achieves maximum convective heat transfer coefficient for heavy-section tool steel dies and superalloy forgings.
Specialized Vacuum Furnace Systems by Thermal Processing Application
Haitem Furnace manufactures high-performance industrial vacuum furnaces engineered for exact metallurgical demands, rigorous temperature thresholds, atmosphere purity, and tailored cooling dynamics. Explore our integrated product portfolio designed specifically for high-density vacuum sintering, precision vacuum quenching, fluxless vacuum brazing, and bright vacuum annealing.
Vacuum Sintering Furnaces with Integrated Debinding
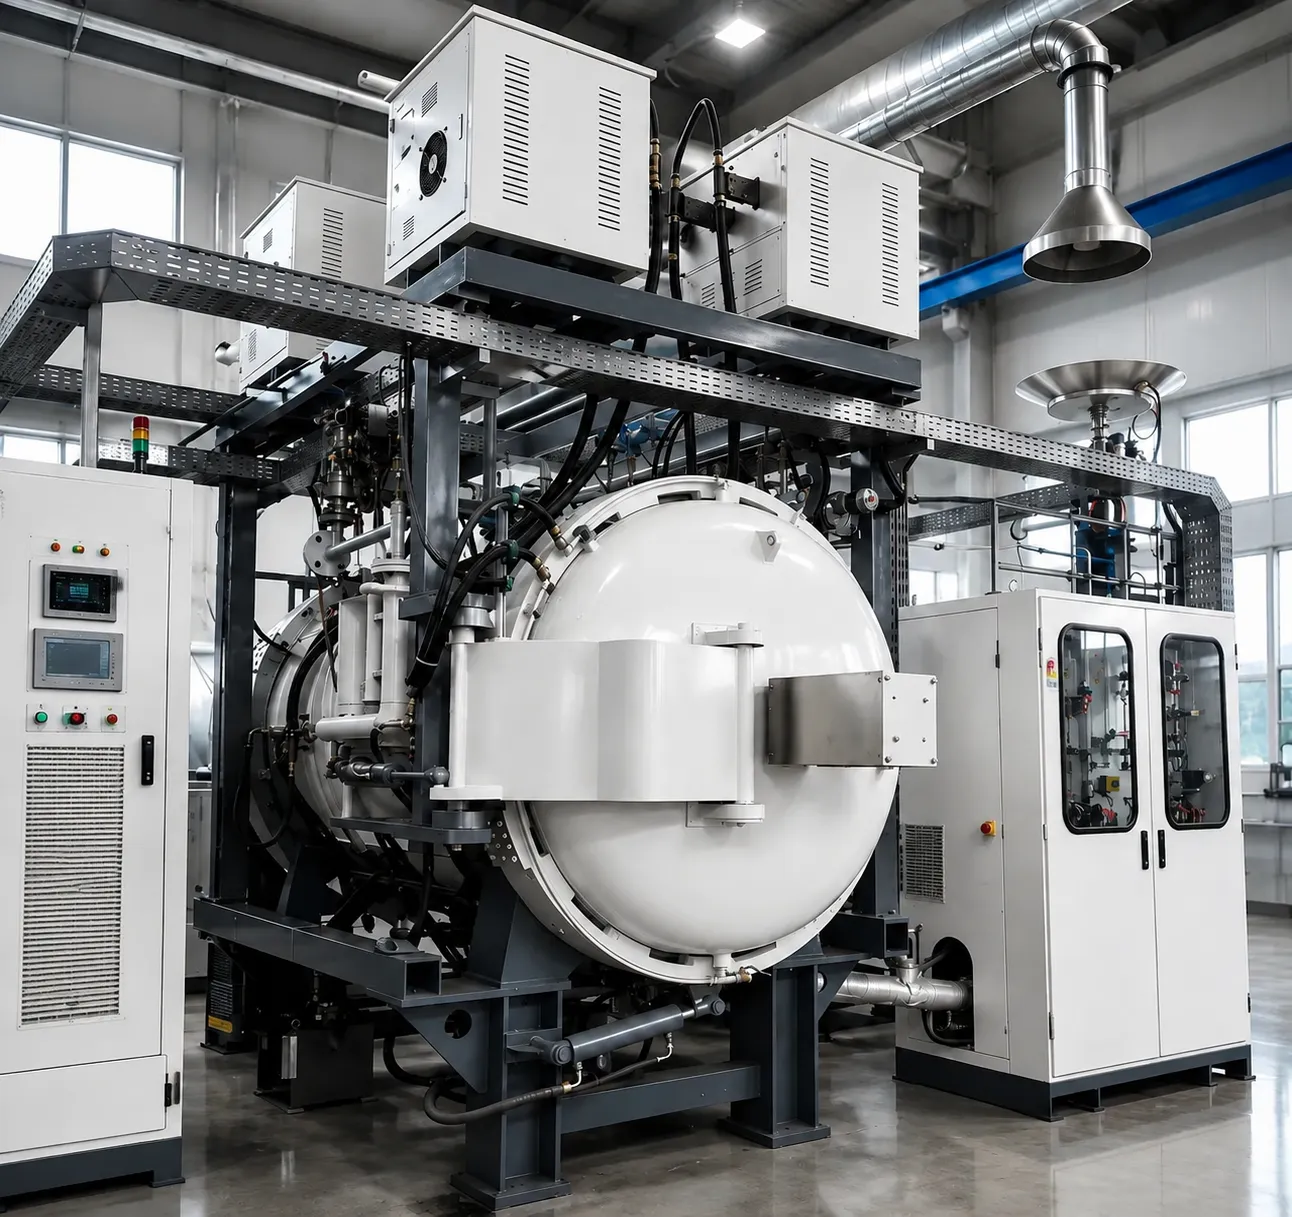
Engineered for powder metallurgy hard alloys, Metal Injection Molding (MIM) parts, and structural ceramics, these specialized systems integrate low-temperature organic binder removal with high-vacuum densification sintering in a single automated thermal cycle. This eliminates intermediate component transfer, prevents surface contamination, and guarantees maximum material density.
Key Engineering Capabilities
- Thermal Debinding Management: Active paraffin wax and binder condensation traps protect vacuum pumps and prevent part cracking during thermal burnout.
- High-Density Sintering: Sustains operating temperatures up to 2400°C under high vacuum (10-4 Pa) or partial pressure inert gas atmospheres.
- Overpressure Sintering (Sinter-HIP): Optional argon gas overpressure up to 10 MPa seals residual micro-porosity for peak mechanical performance.
Cemented Carbides, Tungsten Alloys, MIM Stainless Steel, Titanium, SiC, Al₂O₃, ZrO₂ Ceramics
Vacuum Quenching Furnaces (High-Pressure Gas & Oil)
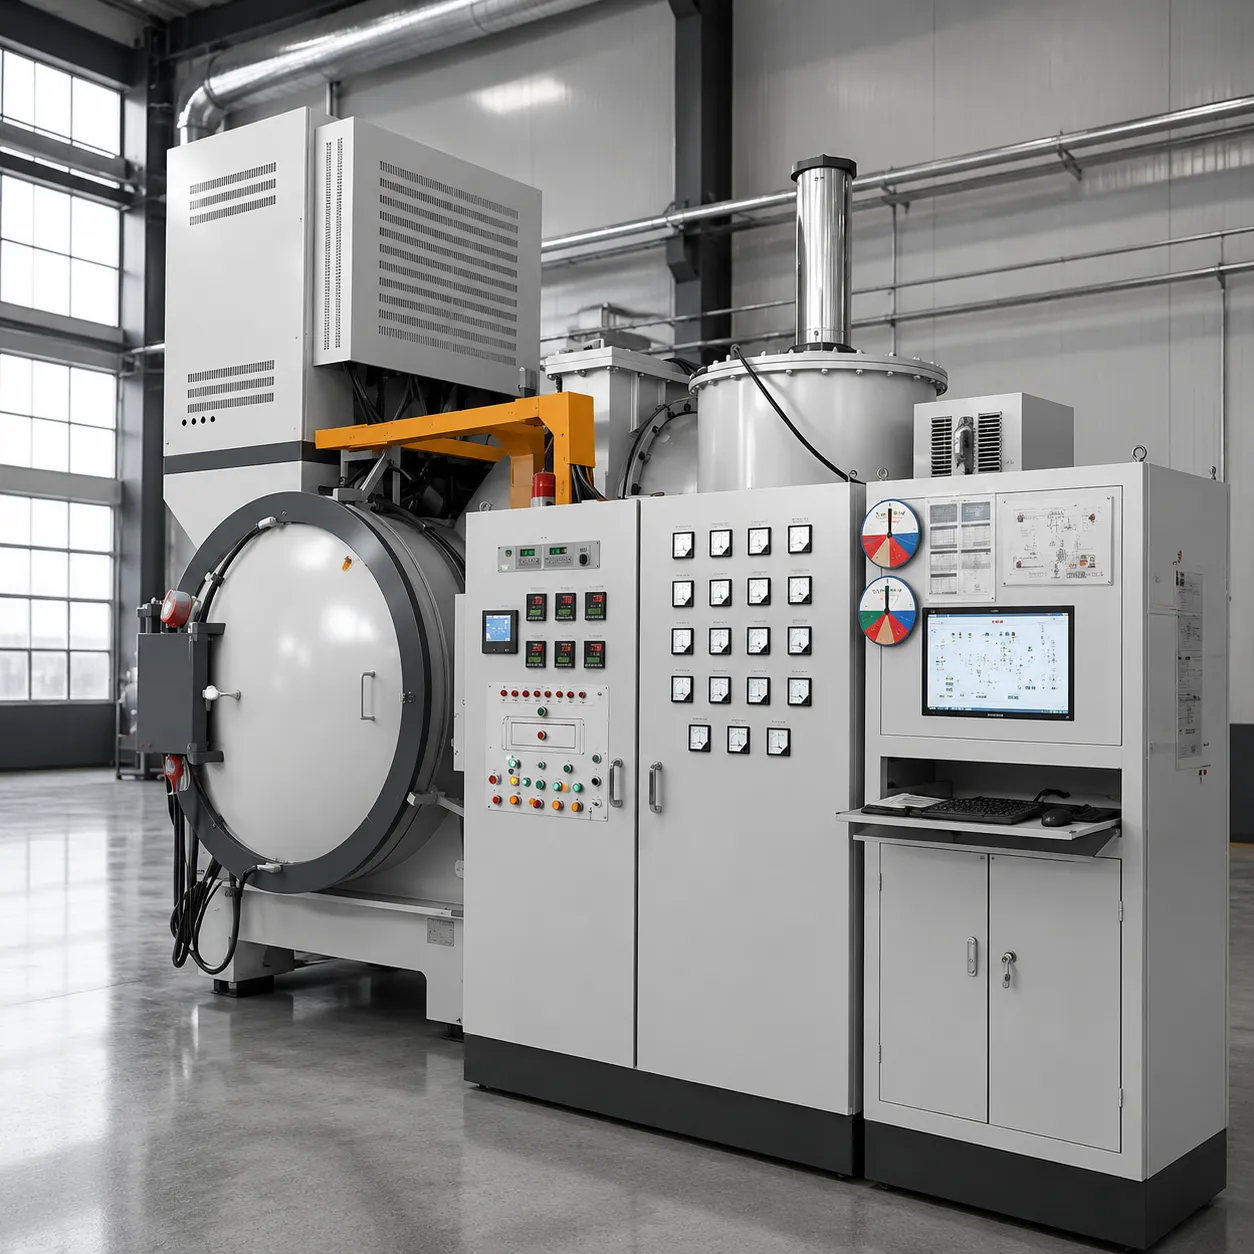
Designed for high-precision hardening, tempering, solution treating, and age hardening of tool steels, die steels, and critical aerospace alloys. Haitem vacuum quenching systems deliver strict phase transformation control, exceptional core hardness, minimum dimensional distortion, and bright, decarb-free surface finishes.
Key Engineering Capabilities
- Directional HPGQ Dynamics: 360-degree high-velocity gas nozzles using N₂, Argon, or Helium at pressures up to 15 bar provide rapid, uniform cooling.
- Integrated Vacuum Oil Quenching: Rapid double-chamber transfer elevators submerge heavy-section components needing ultra-high cooling speeds.
- Distortion Mitigation Technology: Dynamic program-controlled cooling rates minimize thermal stress and microstructural warping in complex dies.
H13 Die Steel, High-Speed Steel (HSS), Martensitic Stainless Steel, Inconel, Heavy Forgings
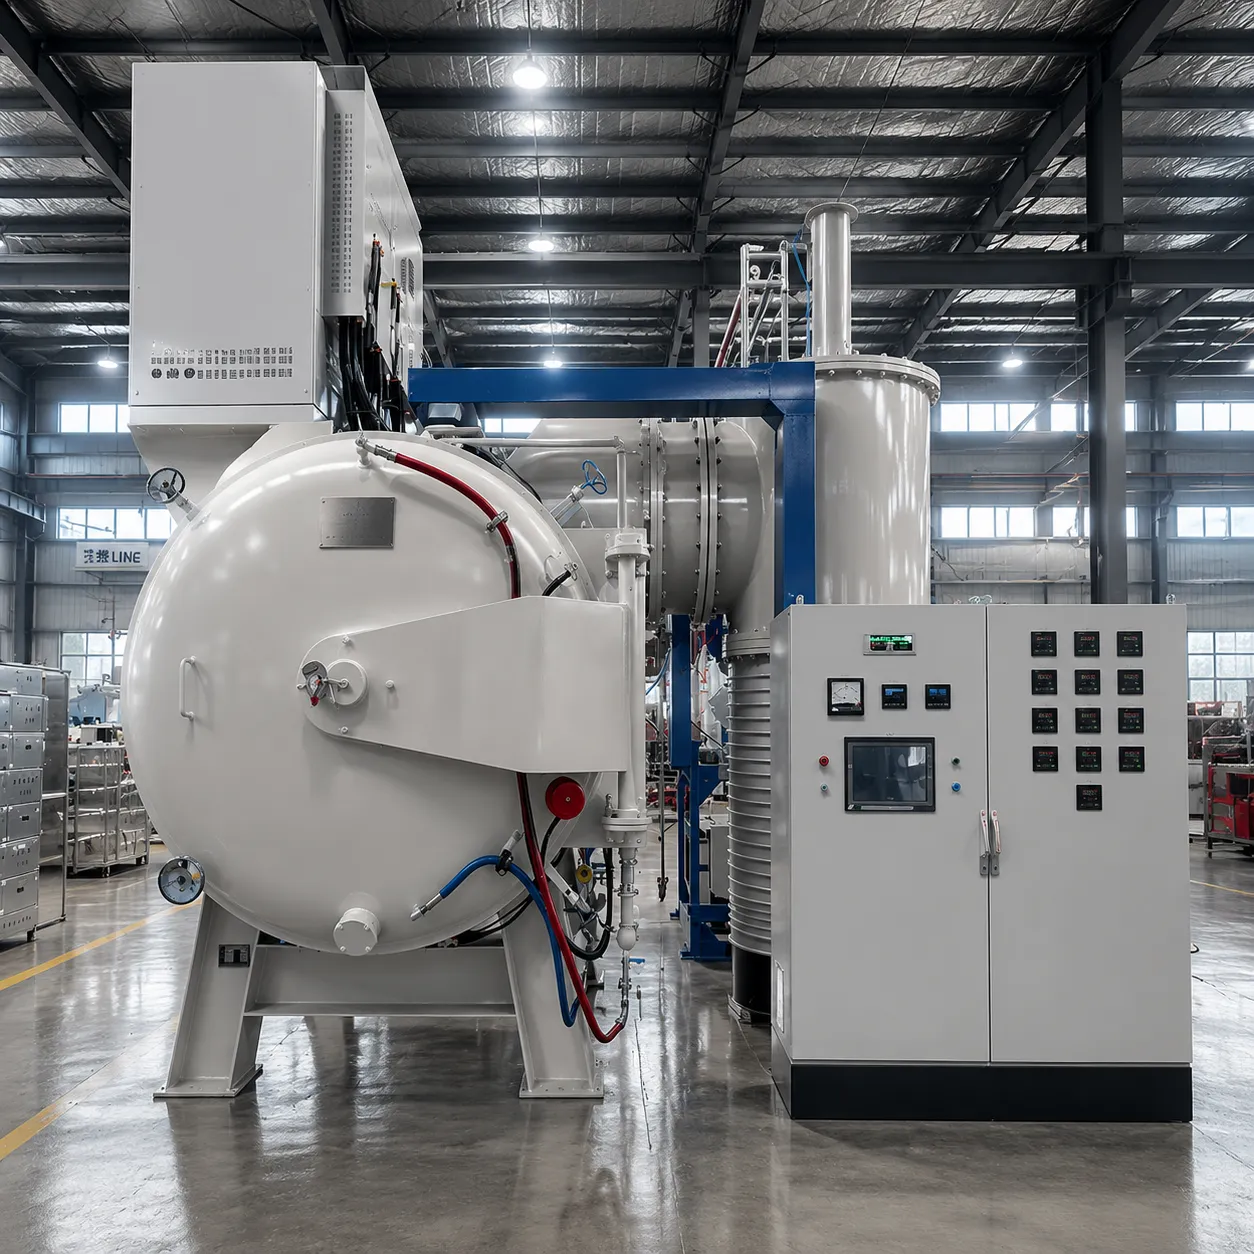
Fluxless High-Vacuum Precision Brazing Furnaces
Purpose-built for clean, fluxless metallic joining of complex aluminum plate-fin heat exchangers, liquid cold plates, and high-temperature aerospace components. Processing in high vacuum breaks surface oxides naturally, producing leak-tight joints without corrosive chemical flux residues.
Key Engineering Capabilities
- Fluxless Chemical-Free Joining: Ultra-high vacuum levels (10-5 Pa) optimize filler alloy capillary action without post-braze acid washing.
- Multi-Zone Thermal Uniformity: Multi-zone independent PID heating guarantees hot zone field variation within ±2°C to prevent joint erosion.
- All-Metallic Hot Zones: Pure molybdenum or tungsten shielding prevents carbon dust contamination during delicate assembly joining.
Aluminum Heat Exchangers, Copper Cold Plates, Stainless Steel Manifolds, Titanium Assemblies
Vacuum Annealing Furnaces (Bright & Soft Magnetic)
Optimized for fine wires, thin strips, cold-rolled metal coils, and soft magnetic alloys. These systems restore ductility, eliminate cold-working stresses, and refine grain alignment to maximize magnetic permeability and overall electrical conductivity.
Key Engineering Capabilities
- Mirror-Bright Surface Finish: Total extraction of oxygen and moisture yields clean, oxidation-free parts directly out of the chamber.
- Magnetic Domain Optimization: Automated slow-cooling curves maximize magnetic permeability (μ) while drastically reducing coercivity (Hc).
- Partial Pressure Hydrogen Sweeping: Optional controlled hydrogen purging strips residual surface carbon for superior electrical properties.
High-Purity Copper & Nickel Wires, Stainless Steel Strips, Permalloy, Silicon Steel, Mumetal Shields
Vacuum Furnace Product Line Comparison Matrix
Compare standard operating thresholds, vacuum levels, and cooling systems across Haitem Furnace product lines to select the right system for your facility.
| System Classification | Max Temp Range | Ultimate Vacuum | Atmosphere Options | Cooling Dynamics | Primary Applications |
|---|---|---|---|---|---|
| Vacuum Debinding & Sintering | 1200°C – 2400°C | 10-1 Pa to 10-4 Pa | High Vacuum, Ar, H₂, N₂ | Natural / Forced Inert Gas | Powder Metallurgy, MIM, Technical Ceramics |
| High-Pressure Gas Quenching (HPGQ) | 1100°C – 1400°C | 10-1 Pa to 10-3 Pa | Partial Pressure N₂, Ar, He | 2 bar – 15 bar Dynamic Directional Gas | Tool & Die Steels, Aerospace Forgings |
| Vacuum Oil Quenching | 1000°C – 1300°C | 10-1 Pa to 10-2 Pa | High Vacuum, Partial Pressure N₂ | Rapid Elevator Oil Submersion | Heavy Structural Steels, Automotive Transmission Gears |
| Fluxless Vacuum Precision Brazing | 600°C – 1300°C | 10-3 Pa to 10-5 Pa | Ultra-High Vacuum, Partial Ar | Internal Inert Gas Circulation | Heat Exchangers, Cold Plates, Aerospace Devices |
| Bright & Magnetic Annealing | 800°C – 1200°C | 10-2 Pa to 10-4 Pa | High Vacuum, Pure H₂ / N₂ Purge | Programmed Linear Rate Cooling | Precision Wires, Soft Magnetic Alloys, Thin Foil Strips |
Require a Custom Configuration for Proprietary Metallurgy Recipes?
Haitem Furnace provides custom non-standard vacuum equipment engineering. Our thermal design group collaborates with your metallurgical engineers to customize hot zone geometry, pump stack capacity, loading configurations, and automated PLC recipes tailored to your exact thermal processing specs.
Precision Vacuum Thermal Processing Solutions for Advanced Manufacturing
Haitem Furnace designs and manufactures high-performance vacuum furnaces engineered for the critical processing demands of modern powder metallurgy, technical ceramic synthesis, aerospace propulsion, and biomedical device manufacturing. By removing atmospheric oxygen, humidity, and volatile hydrocarbons, our equipment delivers zero-oxidation thermal processing, total alloy densification, and exceptional thermal uniformity across complex structural geometries. Supported by our comprehensive manufacturing capabilities, we ensure every system meets exact operational specifications.
High-Purity Sintering & Debinding for MIM and PM Parts
Metal Injection Molding (MIM) and advanced powder metallurgy require meticulous temperature ramping to ensure complete binder removal without disrupting component geometry. Haitem vacuum sintering furnaces integrate active organic trap systems with controlled partial-pressure environments to process stainless steel, titanium, cobalt-chromium, and tungsten heavy alloys free from micro-porosity or intergranular contamination.
By combining thermal debinding with high-temperature vacuum sintering up to 1400°C in a single continuous cycle, our systems drive uniform isotropic shrinkage, optimize mechanical yield strength, and produce near-net-shape components ready for immediate deployment.
- Stainless Steel & Titanium MIM: Prevents interstitial carbon and oxygen absorption while maintaining exact stoichiometric balances.
- Cobalt-Chromium & Tool Alloys: Yields bright, oxide-free surface finishes direct from the hot zone, eliminating secondary surface cleaning.
Ultra-High Temperature Vacuum Annealing & Sintering for Ceramics
Synthesizing non-oxide technical ceramics, Silicon Carbide (SiC), high-purity graphite, and quartz substrates demands ultra-clean, high-vacuum environments and extreme thermal capability. Haitem advanced ceramics furnace solutions utilize high-purity graphite, tungsten, or molybdenum heating elements custom-engineered for continuous high-vacuum operation up to 2400°C.
These specialized thermal processing systems stop chemical degradation during recrystallization, reaction sintering, and vacuum degassing, fulfilling the stringent purity standards required for semiconductor wafer processing fixtures and heat dissipation substrates.
- Silicon Carbide (SiC) & Nitride Ceramics: Supports solid-state reaction sintering in high-vacuum or ultra-pure argon/nitrogen atmospheres.
- Semiconductor Vacuum Annealing: Eliminates trace metallic impurities in graphite, quartz, and silicon components for cleanroom compatibility.
Zero-Oxidation High-Pressure Gas Quenching for Aerospace Steels
High-alloy die steels, forging tools, and mission-critical aerospace turbine components require maximum surface hardness and core toughness without geometric distortion or scaling. Haitem vacuum quenching furnace configurations incorporate 360-degree directional gas nozzles powered by pressurized nitrogen, argon, or helium up to 15 bar for fast, programmable cooling.
By replacing conventional oil quenching with controlled high-pressure gas cooling, our systems achieve full martensitic transformation while keeping component surfaces completely scale-free, eliminating post-heat treatment pickling and abrasive bead blasting.
- Die & Tooling Steels (H13, D2, P20): Achieves deep, repeatable hardness profiles with minimal residual thermal stress and distortion.
- Turbine Blades & Superalloys: Multi-zone thermal control guarantees tight chamber temperature uniformity within ±3°C throughout hold cycles.
Contamination-Free Vacuum Brazing & Annealing for Medical Alloys
Titanium orthopedic implants, sub-millimeter surgical instruments, and medical-grade stainless steel assemblies demand pristine, oxide-free surfaces and high-integrity joint bonds. Haitem vacuum brazing furnaces operate under high-vacuum conditions down to 10⁻⁵ Pa, delivering fluxless metal joining that eliminates corrosive chemical residues.
Our specialized medical-grade vacuum thermal equipment supports strict ISO 13485 biocompatibility requirements, encouraging superior capillary action during brazing filler flow and providing stress-free vacuum bright annealing for intricate surgical devices.
- Titanium Orthopedic Implants: High-vacuum fluxless joining ensures exceptional mechanical shear strength and long-term biocompatibility.
- Surgical Micro-Instruments: Controlled vacuum stress-relief annealing prevents micro-structure embrittlement and work-hardening defects.
Vacuum Furnace Specification & Custom Hot Zone Engineering
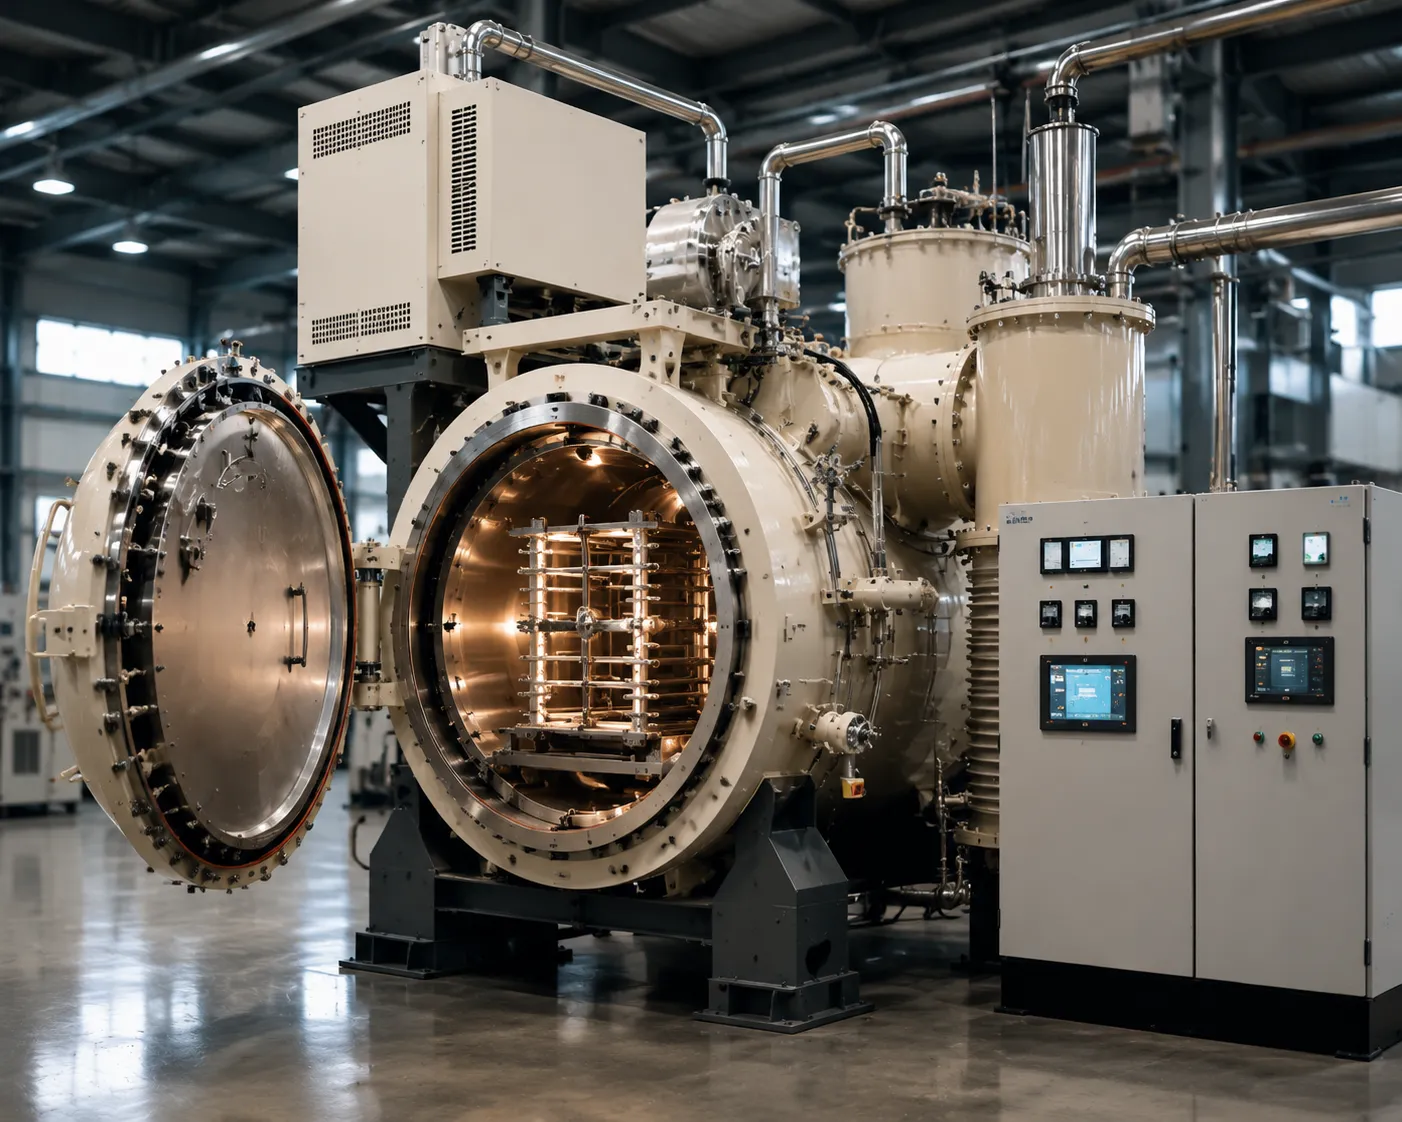
Selecting the ideal vacuum thermal processing configuration depends on material chemical activity, target temperature thresholds, and cooling velocity requirements. Learn more about us and how Haitem thermal engineering teams work alongside global manufacturers to specify optimum vacuum pumping stacks, chamber dimensions, and hot zone materials—including molybdenum, tungsten, and high-purity graphite elements—for reliable batch repeatability.
Sector Application Technical Matrix
Cross-industry technical reference for materials, vacuum thermal cycles, and key performance benchmarks.
| Industry Sector | Target Materials | Primary Vacuum Process | Atmosphere / Cooling Method | Key Performance Metric |
|---|---|---|---|---|
| Powder Metallurgy & MIM | 316L, 17-4PH, Ti-6Al-4V, CoCr Alloys | Debinding & High-Density Powder Metallurgy Vacuum Sintering | Partial pressure Ar/N2 + forced gas cooling | 99.5% Theoretical Density |
| Semiconductors & Technical Ceramics | Silicon Carbide (SiC), Graphite, Quartz, AlN | Semiconductor Vacuum Annealing & Ultra-High Temp Sintering | High vacuum down to 10⁻⁵ Pa / Inert gas purge | 2400°C Max Temperature |
| Aerospace & Tooling Dies | H13, D2, Inconel 718, Titanium Superalloys | Zero-Oxidation High-Pressure Gas Quenching (HPGQ) | 2 bar – 15 bar N2/Ar 360° directional gas stream | Zero Scale & Minimal Distortion |
| Medical Device Manufacturing | Titanium Implants, Nitinol, Surgical Stainless | Fluxless Vacuum Brazing & Bright Vacuum Annealing | Ultra-clean high vacuum environment | 100% Biocompatible Finish |
Key Technological Benefits & Performance Metrics
Engineered to eliminate surface oxidation, ensure precise temperature uniformity, and deliver repeatable, high-yield thermal processing across demanding industrial applications.
Mirror-Bright Finish
Achieve clean atmosphere control that guarantees bright, oxidation-free parts—eliminating post-process acid pickling or mechanical grinding.
Precise Thermal Control
Multi-zone independent PID heating ensures precise temperature uniformity throughout the hot zone, eliminating hotspots across heavy loads.
High-Pressure Gas Quench
Controlled gas quenching delivers rapid, highly uniform cooling that significantly reduces thermal stress and distortion in complex tooling.
Automated Execution
Zero harmful exhaust emissions, optimized thermal insulation, and automated single-touch PLC recipe management ensure consistent quality.
Engineered for Superior Metallurgy & Low Operational Cost
Haitem Furnace combines advanced clean atmosphere control with intelligent multi-zone thermal management to maximize component yield and lower overall operating expenses.
Eliminate Secondary Finishing Costs
High-vacuum processing delivers mirror-bright metal surfaces directly out of the chamber, eliminating secondary polishing or chemical treatments.
Prevent Distortion in Intricate Geometries
Directional high-pressure gas quenching maintains tight geometric tolerances and minimizes post-heat-treatment dimensional corrections.
Sustainable & Energy-Efficient Operation
Advanced thermal shielding and low radiation heat loss help facilities meet environmental standards while reducing energy consumption.
Technical Selection Criteria: How to Choose a Vacuum Furnace
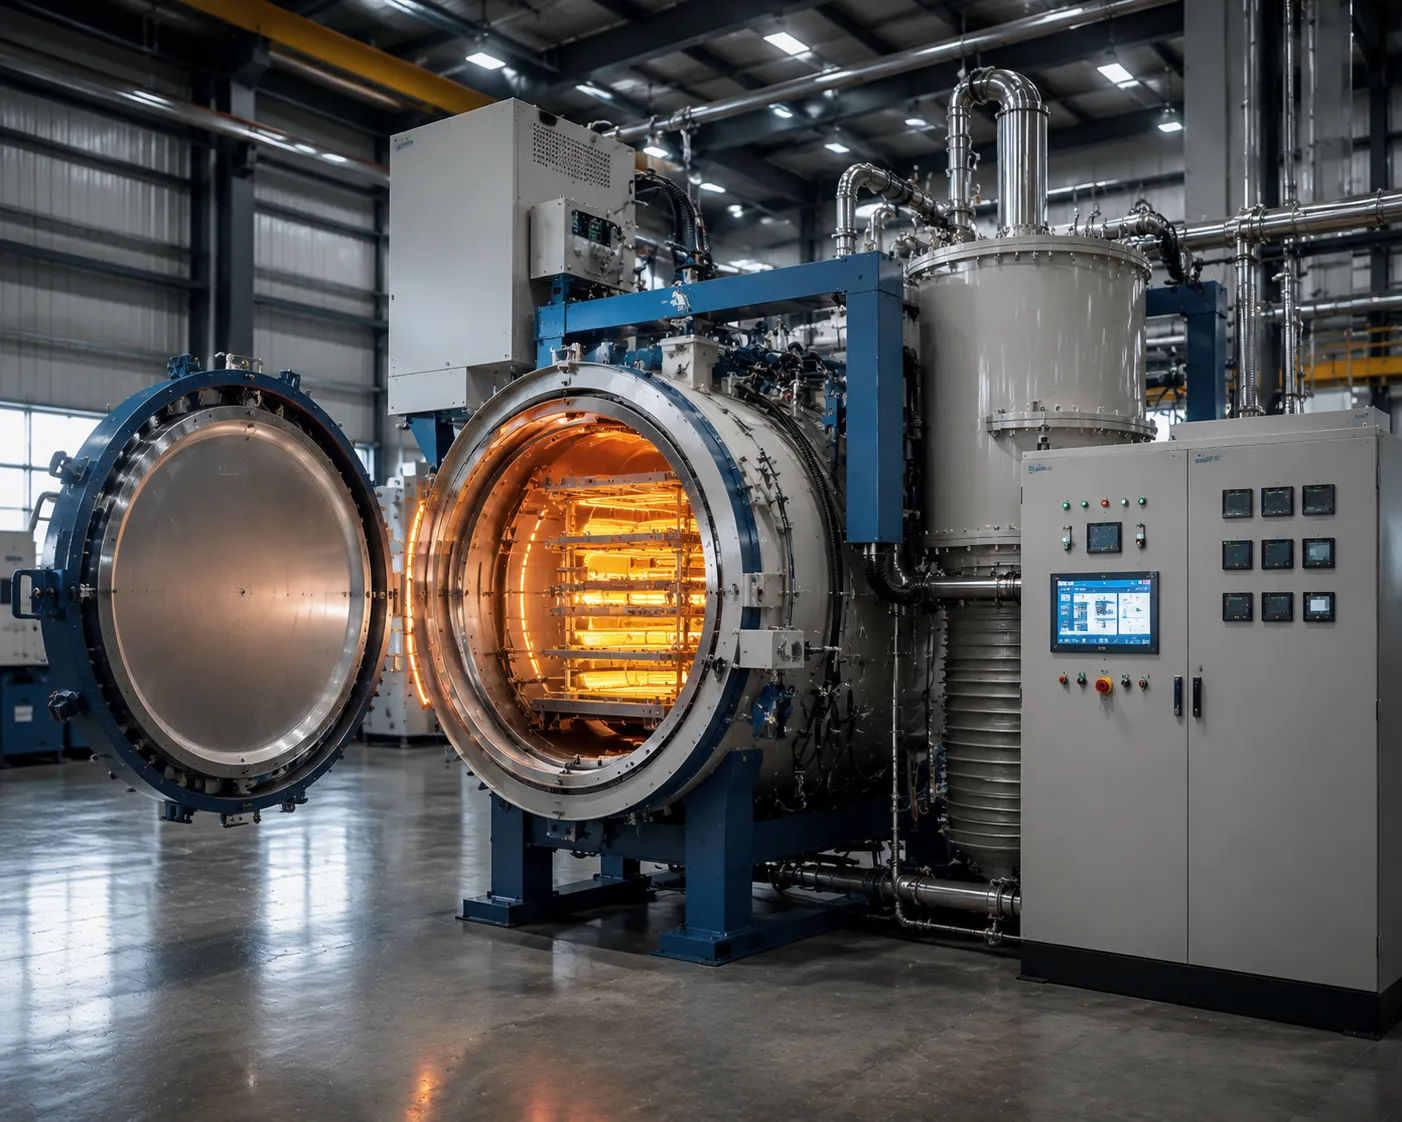
Selecting the optimal industrial vacuum furnaces requires a systematic evaluation of operating temperatures, vacuum levels, hot zone configuration, volumetric dimensions, and quenching dynamics. Haitem Furnace utilizes a rigorous four-stage engineering framework to help metallurgy teams specify equipment tailored to exact vacuum furnace specifications, alloy chemistries, and high-throughput production targets.
Maximum Operating Temperature and Heating Element Pairing
Process temperature requirements define both heating element composition and hot zone insulation design. Industrial thermal processing cycles generally fall into three operating temperature thresholds:
- 1200°C Operating Threshold: Standard tool steel hardening, tempering, solution treating, and copper or silver brazing. Typically utilizes high-density graphite elements or nickel-chromium alloy heating structures with rigid graphite felt insulation.
- 1600°C Operating Threshold: High-alloy tool steel hardening, stainless steel debinding and sintering, and nickel-based superalloy heat treatment requiring precise thermal control.
- 2400°C Operating Threshold: Ultra-high temperature vacuum processing for refractory metals, silicon carbide ceramics, carbon-carbon composites, and graphite graphitization.
Hot Zone Configuration: Graphite vs. Molybdenum/Tungsten
Graphite Hot Zones provide outstanding thermal shock resistance, lower capital expenditure, and robust mechanical longevity. However, potential micro-carburization must be evaluated for carbon-sensitive alloys. Molybdenum and Tungsten All-Metallic Hot Zones eliminate carbon contamination entirely, making them mandatory for titanium aerospace parts, medical implants, nuclear alloys, and semiconductor processing.
Vacuum Level Assessment and Pumping Architecture
Establishing the target vacuum pressure prevents intergranular oxidation, evacuates organic binder volatiles, and promotes surface oxide reduction based on alloy chemical reactivity.
- Rough Vacuum (10 Pa): Suitable for basic thermal processing, stress relief, and processes employing continuous inert gas partial-pressure flushing to suppress element volatilization.
- High Vacuum (10⁻³ Pa): Essential for bright hardening, fluxless aluminum or copper brazing, and powder metallurgy sintering. Achieved by integrating mechanical backing pumps (rotary vane or dry screw) with Roots blowers or oil diffusion pumps.
- Ultra-High Vacuum (10⁻⁵ Pa): Required for highly reactive alloys including titanium, zirconium, niobium, and specialty aerospace superalloys. Configured with high-speed turbomolecular pumping systems.
Backing and Booster Pump Integration
Pairing oil-free dry screw backing pumps with high-displacement Roots boosters ensures rapid vacuum roughing, protecting sensitive alloy surfaces from hydrocarbon backstreaming during continuous production cycles.
Hot Zone Volumetric Calculation and Hearth Weight Capacity
Proper chamber sizing maintains strict thermal uniformity limits, accommodates charge fixture dimensions, and guarantees hearth structural integrity under high-density loads.
- Effective Uniform Work Zone: Hot zone dimensions must guarantee that all workpieces reside strictly within certified ±3°C or ±5°C temperature uniformity limits in compliance with AMS 2750 or CQI-9 specifications.
- Hearth Rail Loading Ratings: Heavy-duty support rails engineered from molybdenum, silicon carbide, or CFC composites support heavy payloads at elevated operating temperatures without creep or structural deflection.
- Quenching Spatial Clearance: Maintaining optimal clearance between part fixtures and chamber walls facilitates uniform, high-velocity gas distribution during rapid cooling.
Multi-Zone Heating Element Control
Extended volumetric chambers utilize multi-zone independent PID power controllers to compensate for end-wall radiation loss and maintain tight temperature uniformity throughout dense charge loads.
Cooling Method Selection and High-Pressure Gas Quenching
Cooling velocity directly dictates core hardness depth, microstructural phase transformation, grain growth control, and post-process dimensional distortion.
- Natural Furnace Cooling: Unforced radiative vacuum cooling or static partial-pressure cooling, best suited for thermal stress relief, ceramic sintering, and magnetic annealing cycles.
- Forced Gas Quenching (2 bar to 15 bar): High-pressure forced gas circulation using 360-degree directional nozzles. Achieves cooling rates comparable to oil quenching while delivering completely clean, bright parts.
- Quenching Gas Mediums: Nitrogen (N₂) for standard tool steels; Argon (Ar) for titanium alloys and superalloys sensitive to nitriding; Helium (He) for maximum heat transfer velocity in thick-section die steels.
Controlled Distortion Management
Programmable frequency-controlled gas blowers enable dynamic cooling ramps, minimizing thermal gradients and preventing distortion in complex tool dies and thin-walled structural components.
Matching Alloy Families with Vacuum Furnace Specifications
Selecting mismatched furnace options can result in surface decarburization, intergranular oxidation, or inadequate core hardness transformation. Haitem Furnace customizes hot zone configuration, vacuum pumping systems, and gas quenching pressures based on exact metallurgy specifications.
1000°C – 1250°C | Graphite Hot Zone | High Vacuum (10⁻³ Pa) | 6–10 bar N₂ Gas Quench
1100°C – 1400°C | All-Metallic Hot Zone | Ultra-High Vacuum (10⁻⁵ Pa) | High-Purity Argon Quench
1600°C – 2400°C | High-Purity Graphite / Tungsten | High Vacuum (10⁻³ Pa) | Controlled Furnace Cool
600°C – 1150°C | Metallic or Graphite Hot Zone | High Vacuum (10⁻⁴ Pa) | Partial-Pressure Inert Purge
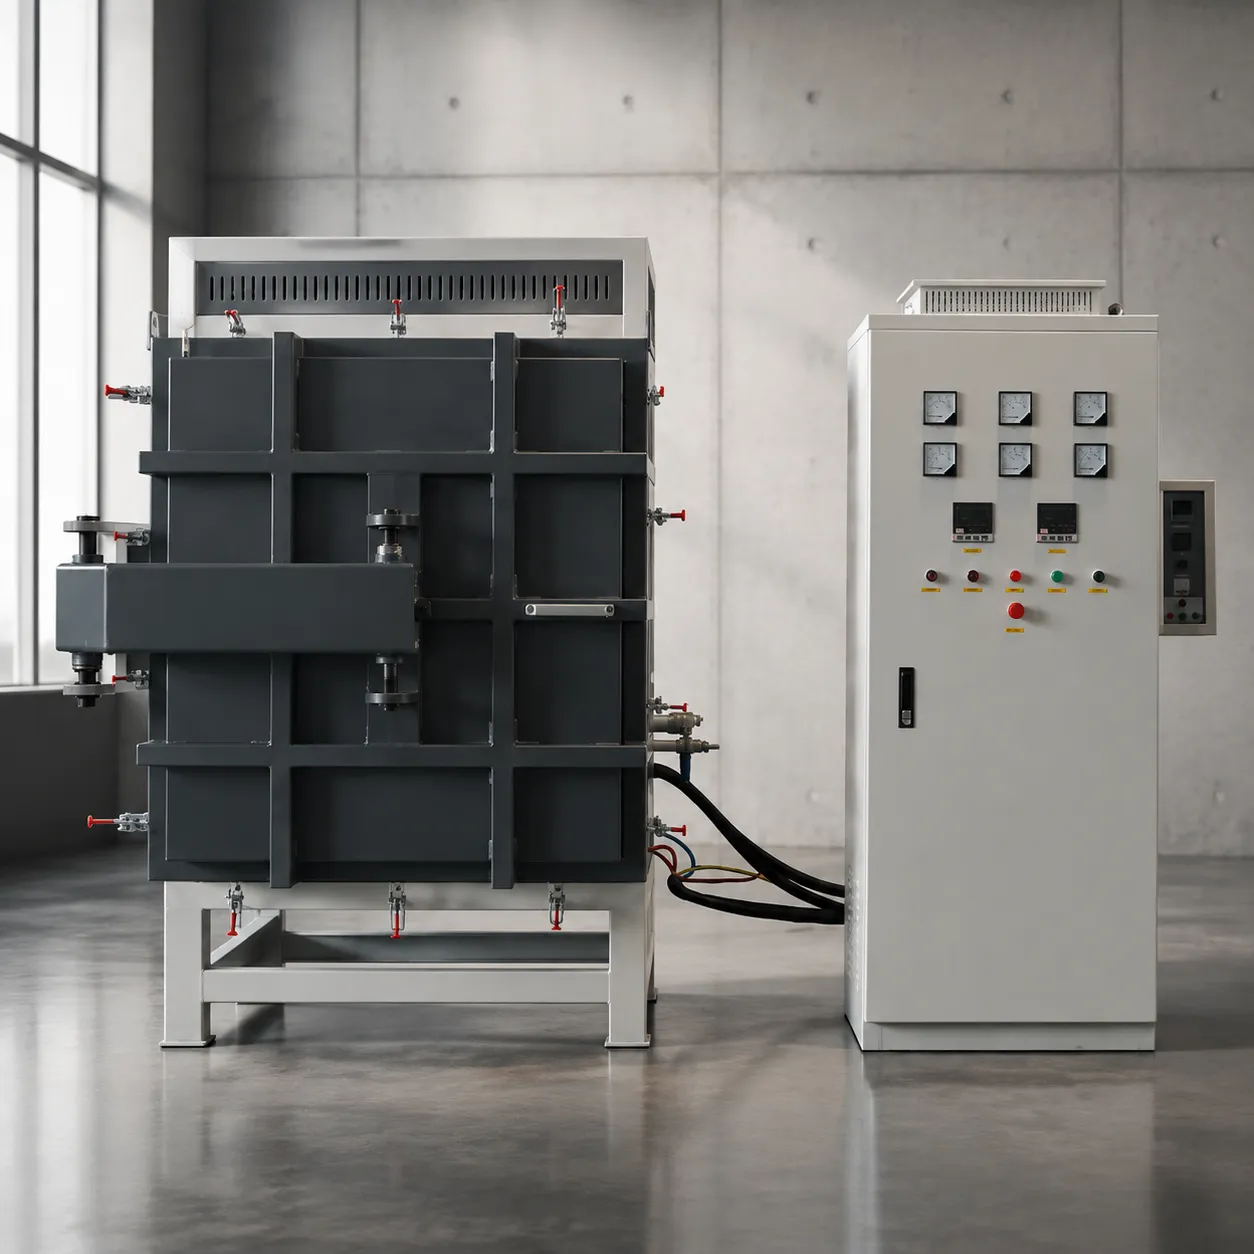
Technical Vacuum Furnace Specification Comparison Matrix
| Design Parameter | Graphite Hot Zone System | All-Metallic (Moly/Tungsten) System | Engineering Selection Rationale |
|---|---|---|---|
| Max Temperature Limits | Up to 2400°C (Continuous) | 1350°C (Moly) / 2400°C (Tungsten) | Graphite provides superior structural stability and thermal longevity at extreme ultra-high temperatures. |
| Atmospheric Cleanliness | Low outgassing; potential micro-carburization | Zero carbon outgassing; mirror-bright surface finish | Metallic hot zones are mandatory for titanium, medical implants, nuclear components, and semiconductor processing. |
| Ultimate Vacuum Capability | 10⁻¹ Pa to 10⁻³ Pa | 10⁻³ Pa to 10⁻⁵ Pa | Metallic systems allow faster pump-down times to ultra-high vacuum thresholds due to lower material outgassing. |
| Gas Quenching Resilience | Exceptional thermal shock resistance (up to 15 bar) | Requires controlled thermal ramps (up to 10 bar) | Graphite withstands rapid gas pressure transitions and extreme thermal shocks without structural cracking. |
| Capital & Operating ROI | Lower initial cost; economical replacement elements | Higher initial investment; careful handling required | Graphite yields maximum ROI for tool steel hardening, tempering, and high-volume powder metallurgy facilities. |
Tailored Vacuum Furnace Engineering by Haitem Furnace
Specifying the ideal vacuum furnace requires balancing metallurgical thermal profiles, vacuum levels, hot zone configuration, hearth structural capacities, and gas quenching velocity. Haitem Furnace engineers conduct custom thermal field simulations, hearth static load stress analyses, and vacuum pumping speed calculations for every unit. Contact our engineering team to review your specific production parameters and receive a tailored technical equipment proposal.
Vacuum Furnace Technical FAQ & Selection Guide
Optimizing industrial thermal processing requires aligning metallurgical specifications with hot zone materials science, vacuum pumping dynamics, and cooling efficiency. Below are detailed technical answers to key engineering decisions encountered during vacuum furnaces evaluation, thermal process design, and equipment procurement.
Molybdenum Metallic Hot Zone vs. Graphite Hot Zone Selection Criteria
Comparing structural integrity, operating temperatures, atmosphere purity, and carbon sensitivity.
Choosing between an all-metallic molybdenum hot zone and a rigid graphite fiber hot zone is a fundamental decision in vacuum furnace design. This choice determines process atmosphere cleanliness, maximum operating temperature, thermal insulation efficiency, and long-term operating costs.
All-Metallic Hot Zone (Molybdenum / Tungsten)
- Atmosphere Purity: Guaranteed zero carbon contamination; necessary for strict ultra-clean heat treatment.
- Optimal Substrates: Titanium alloys, medical orthopedic implants, high-purity stainless steel, superalloys, and refractory metals.
- Peak Temperature: Molybdenum supports up to 1600°C; Tungsten configurations reach up to 2400°C.
- Vacuum Range: Operates efficiently in high to ultra-high vacuum levels down to 10⁻⁵ Pa.
Graphite & C-C Composite Hot Zone
- Thermal Dynamics: Excellent thermal shock resistance, rapid heating cycles, and high dimensional stability under thermal stress.
- Optimal Substrates: Tool and die steels, high-speed steels, powder metallurgy alloys, MIM parts, silicon carbide, and industrial ceramics.
- Peak Temperature: Routinely operates up to 2400°C with high structural rigidity.
- Operational Cost: Lower initial investment and economical heating element replacement over extended production runs.
Vacuum Gas Quenching vs. Oil Quenching: Key Differences
Evaluating cooling velocity, workpiece distortion, surface cleanliness, and alloy hardenability requirements.
Quenching in a vacuum furnace converts austenite to martensite while managing mechanical properties and controlling dimensional change. Selecting High-Pressure Gas Quenching (HPGQ) or Vacuum Oil Quenching depends primarily on alloy hardenability and part geometry.
| Performance Metric | High-Pressure Gas Quenching (HPGQ) | Vacuum Oil Quenching |
|---|---|---|
| Cooling Medium | High-purity Nitrogen, Argon, or Helium gas (2 bar to 15 bar pressure) | Degassed, low-vapor-pressure specialized vacuum quenching oil |
| Surface Cleanliness | Bright finish; requires no post-quench degreasing or chemical washing | Requires post-quench washing and degreasing to remove oil residue |
| Distortion Control | Lower distortion using dynamic 360-degree directional gas nozzles | Higher thermal shock risk due to vapor blanket phase changes during cooling |
| Cooling Velocity & Cycle Time | Controllable cooling speed optimized for air-hardening and medium-alloy steels | Ultra-fast cooling rate for low-hardenability carbon and low-alloy steels |
| Environmental Impact | Zero oil mist emissions, clean operation, integrated gas recovery available | Requires waste oil management, filtration systems, and exhaust controls |
Key Factors Influencing Ultimate Vacuum Levels & System Maintenance
Managing chamber outgassing, pumping stage configuration, leak rate testing, and preventive oil management.
Reaching and maintaining target vacuum levels (from rough vacuum at 10 Pa down to ultra-high vacuum at 10⁻⁵ Pa) depends on pumping system design, chamber structural integrity, and regular preventive maintenance.
Primary Variables Affecting Vacuum Performance:
Water vapor adsorbed on cold vessel walls during loading is the main gas load during evacuation. Bake-out cycles and inert gas purges help reduce outgassing.
Matching sizing ratios between primary backing pumps (screw or rotary vane), Roots mechanical boosters, and secondary high-vacuum pumps (diffusion or turbomolecular).
Worn Viton O-rings or trapped air pockets in blind screw holes release gas slowly, preventing the system from reaching ultimate vacuum targets.
Contaminated mechanical pump fluid reduces pumping speed and increases oil backstreaming into the heating chamber during hold cycles.
Preventive Maintenance Schedule for Vacuum Systems:
- Weekly Inspection: Check mechanical pump oil sight glasses for cloudiness, moisture emulsion, or fluid loss. Replace contaminated pump fluid immediately.
- Monthly Leak Testing: Perform rate-of-rise leak testing with the chamber isolated. A well-maintained vessel should maintain a leak rate under 0.5 Pa/hour.
- Quarterly Seal Maintenance: Clean and lubricate door elastomer O-rings using high-vacuum fluoro-silicone grease. Inspect sealing surfaces for scratches or wear.
- Annual High-Vacuum Service: Inspect diffusion pump heaters and jet assemblies or service turbomolecular bearings to maintain consistent 10⁻⁵ Pa performance.
Engineering Custom Vacuum Furnaces for Specialized Alloys
Customizing thermal profiles, multi-zone control systems, dewaxing traps, and specialized gas management.
Standard vacuum furnaces may not meet the specific requirements of advanced aerospace superalloys, technical ceramics, or specialized powder metallurgy recipes. Learn more about us to see how Haitem Furnace designs custom equipment to match specific physical, metallurgical, and production requirements.
Custom Chamber Sizing & Hearth Design
Chamber dimensions configured for unique workpiece geometries, hearth load capacities up to 10 tons, and flexible loading configurations (horizontal or bottom-loading elevator designs).
Multi-Zone PID Temperature Control
Independent heating zones maintaining temperature uniformity within ±1°C or ±3°C across complex hearth layouts, compliant with AMS 2750G pyrometry standards.
Integrated Debinding & Condensation Traps
Specialized thermal debinding traps and multi-stage filters for MIM or ceramic sintering that capture off-gassed binders and prevent hot zone contamination.
Need Custom Furnace Sizing or Process Verification?
Contact Haitem Furnace thermal processing specialists for sizing evaluations, process simulations, or a custom equipment proposal tailored to your metallurgical requirements.
Ready to Optimize Your Industrial Thermal Processing?
Partner with Haitem Furnace to engineer a custom vacuum furnace solution tailored to your exact metallurgical requirements. Receive a comprehensive process evaluation, hot zone sizing analysis, and technical proposal for your facility.
24-Hour Engineering Response
Receive technical feedback and system configuration guidance within 24 business hours.
Free Material Sample Testing
Verify metallurgical results and thermal profiles inside the Haitem Thermal Testing Laboratory.
Start Your Custom Sizing Analysis
Select an option below to consult directly with our industrial furnace manufacturer team.