Industrial Sintering Process Guide & Advanced Thermal Technology
Master thermal profile management, debinding cycles, and atmospheric isolation for powder metallurgy, MIM, and technical ceramics. Learn more about us and our industrial heating capabilities.
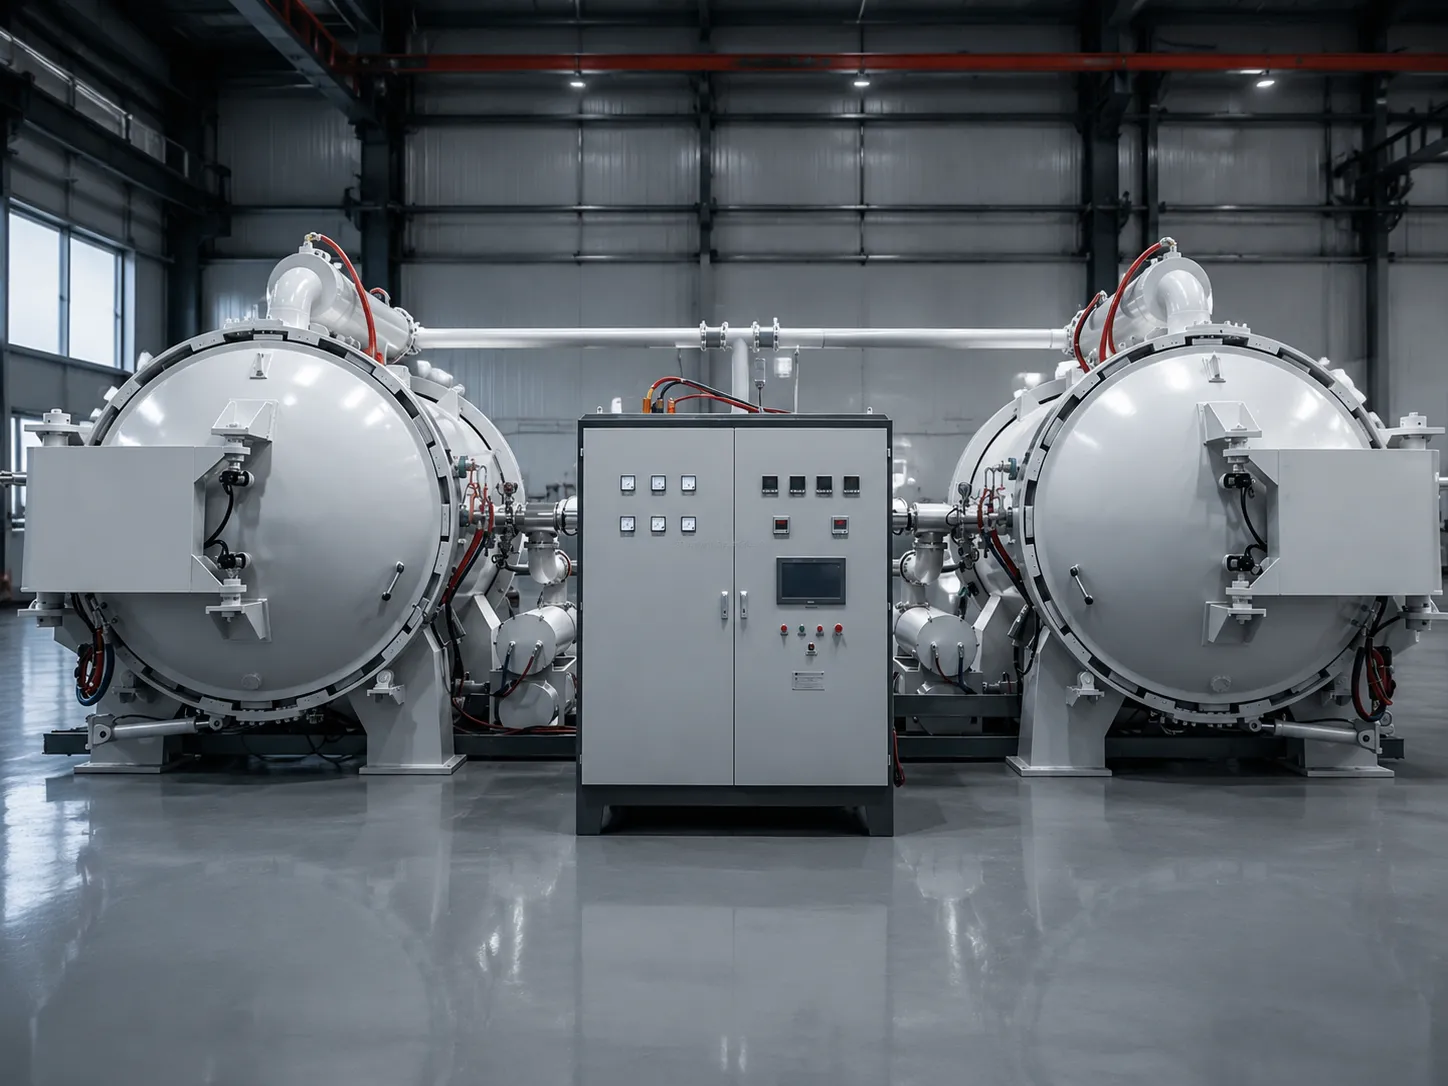
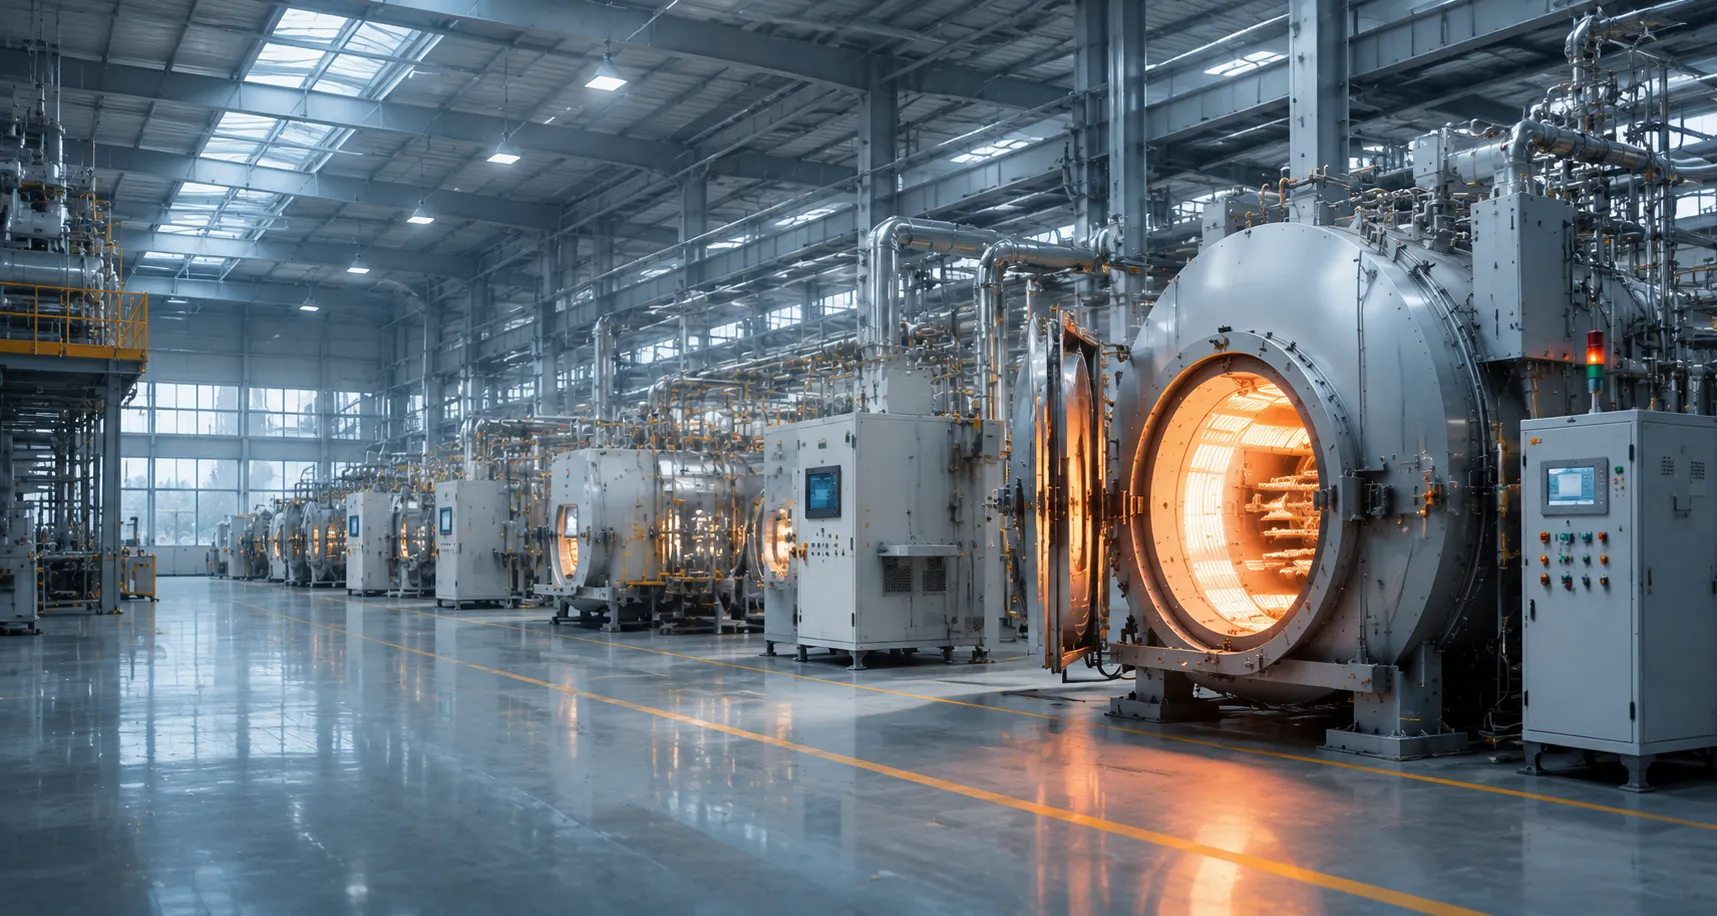
Vacuum Hot Zone Architecture
Precision heat distribution and microstructural pore-elimination for high-density components.
Sintering Temperature Profile & Thermal Lifecycle Analysis
Mastering industrial powder metallurgy, metal injection molding (MIM), and technical ceramic consolidation requires precise control over the thermal processing lifecycle. Precision management of temperature ramp rates, atmospheric dynamics, and thermal dwell zones prevents structural distortion, eliminates internal porosity, and yields peak mechanical density.
Time-Temperature-Atmosphere Profile
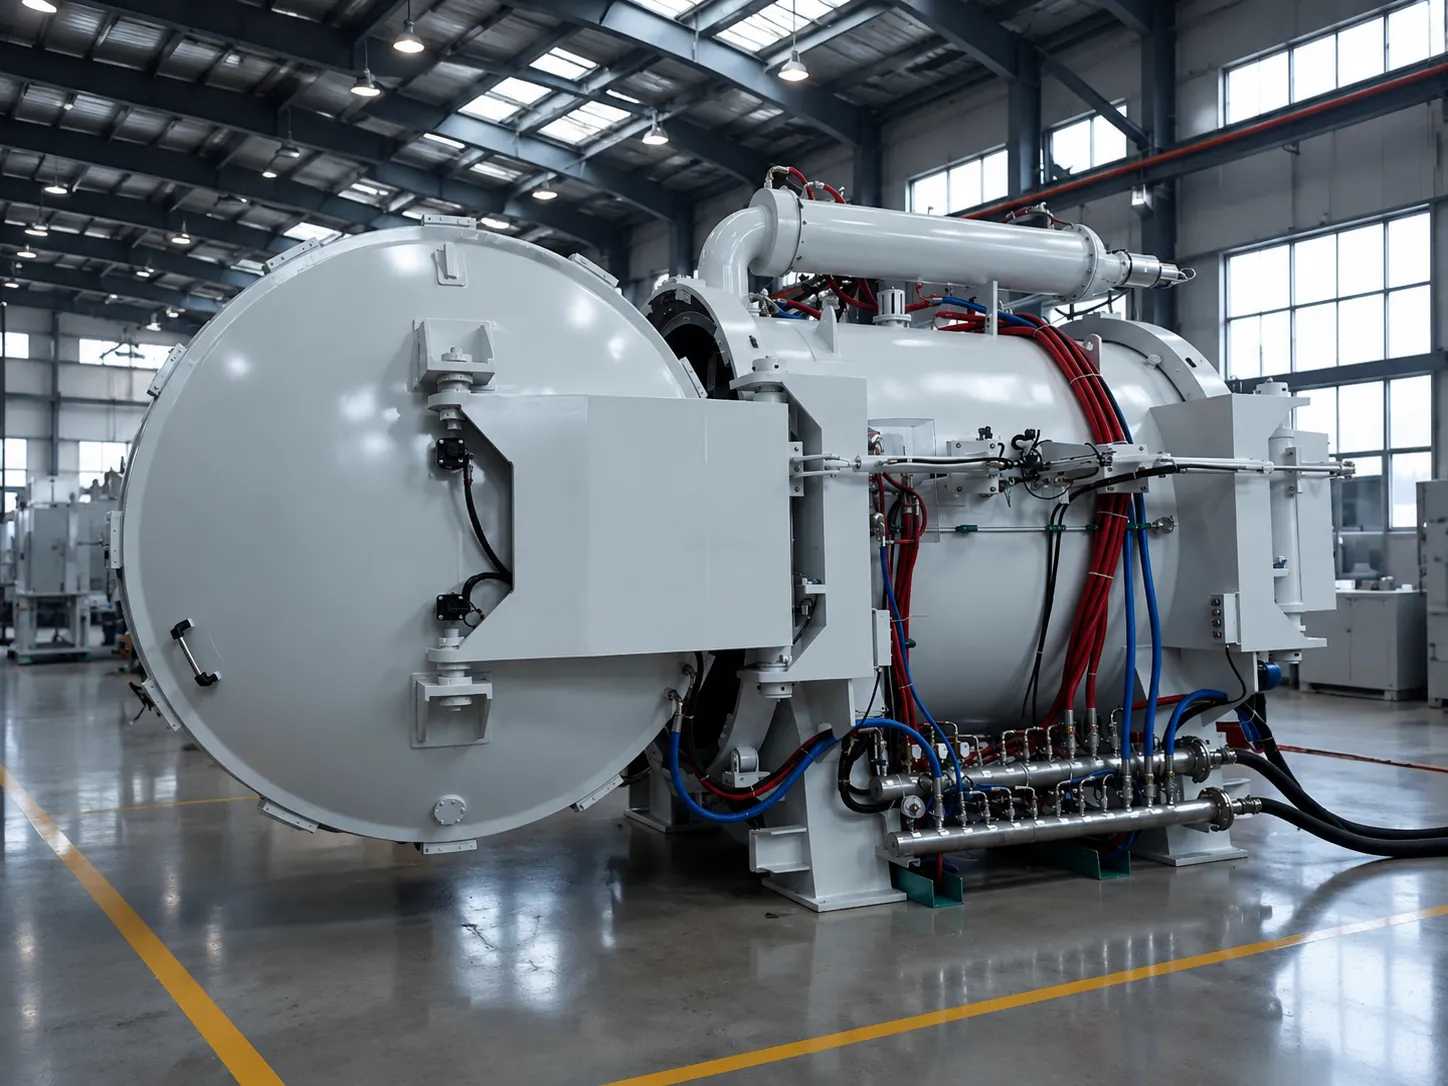
Haitem high-vacuum hot zone internal geometry featuring multi-layer molybdenum heating elements and uniform thermal distribution.
Debinding and Pre-Sintering
Temperature Range: 200°C to 600°CThe debinding and presintering stage focuses on the controlled thermal breakdown, extraction, and evacuation of organic binders, plasticizers, and wax lubricants used during green compact forming. Controlling the temperature ramp rate in this window prevents rapid outgassing pressures that induce internal micro-cracks, surface blistering, or structural distortion.
High-Temperature Consolidation
Temperature Range: 1000°C to 2400°CDuring isothermal high-temperature holding, solid-state diffusion accelerates rapidly across contact points. Mass transport mechanisms—including grain boundary and volume diffusion—drive pore elimination, volumetric shrinkage, and full metallurgical coalescence, transforming porous green bodies into high-density industrial components.
Controlled Cooling and Solidification
Temperature Range: Peak Temp to AmbientThe cooling rate dictates final phase distribution, grain boundary structure, and residual internal stress states. Precision programmed cooling curves mitigate thermal shock, prevent grain coarsening, and guarantee dimensional reproducibility across complex engineered geometries.
Critical Thermal Control Dynamics in Industrial Sintering Profile Engineering
Achieving consistent mechanical integrity and precise dimensional tolerances in industrial powder metallurgy (PM), metal injection molding (MIM), and advanced technical ceramic production depends entirely on the accuracy of your sintering temperature profile. Thermal processing requires total harmony between heating element response, multi-zone temperature uniformity, and gas atmosphere management. A poorly regulated temperature curve introduces non-uniform thermal gradients across the furnace charge, causing differential shrinkage, part distortion, internal voids, and uneven grain boundaries.
Haitem Furnace addresses these critical process dynamics through multi-zone independent heating configurations governed by advanced multi-segment PID controllers. By precisely managing heating rates during sensitive phase transitions—most notably the organic debinding and presintering window between 200°C and 600°C—Haitem thermal processing equipment maintains spatial temperature uniformity within ±1°C across the entire effective hot zone. Our advanced manufacturing capabilities ensure this rigorous thermal field stability eliminates localized thermal stresses, prevents hydrocarbon gas entrapment, and optimizes mass transport kinetics during high-temperature consolidation.
| Process Stage | Target Temp Window | Atmosphere / Vacuum Conditions | Primary Physical Phenomenon | Key Risk Factor |
|---|---|---|---|---|
| Debinding and Pre-Sintering | 200°C to 600°C | Partial Vacuum or Sweeping Inert Gas | Polymer degradation, binder evaporation, & initial necking | Carbon soot contamination & internal micro-blistering |
| High-Temp Consolidation | 1000°C to 2400°C | High Vacuum (10⁻³ Pa) or Pure H₂ / Ar | Atomic diffusion, grain growth, & pore elimination | Dimensional warping, incomplete density, & grain coarsening |
| Controlled Cooling | Peak Temp to Ambient | Pressurized Inert Gas Quenching or Vacuum | Microstructure solidification & stress relaxation | Thermal shock cracking, micro-fissuring, & residual stress |
Custom Thermal Profile Optimization Support
Haitem Furnace engineers assist global clients with material sample testing, debinding and pre-sintering curve development, and custom furnace hot-zone thermal field simulation.
Vacuum Sintering Furnace vs. Controlled Atmosphere Sintering
Selecting the optimal consolidation environment is critical to achieving near-theoretical density, phase purity, and dimensional reproducibility. Compare high-vacuum thermal processing with controlled gas atmospheres to determine the ideal configuration for your material requirements.
Vacuum Sintering Furnace Systems
Operate under deep vacuum furnaces conditions down to 10-3 Pa to extract volatile contaminants, prevent oxidation at elevated temperatures, and promote rapid grain boundary diffusion for void-free consolidation.
Core Technical Advantages
- Near-Total Micro-Porosity Elimination: Evacuates trapped pore gases to achieve relative densities exceeding 99% of theoretical limits.
- Zero Oxidation Risks: Prevents oxygen pickup and grain boundary degradation in highly reactive metals and oxygen-sensitive alloys.
- High-Purity Thermal Degassing: Rapidly volatilizes organic binders and lubricant residues without leaving residual carbon contamination.
Target Material Categories
Controlled Atmosphere Sintering Systems
Utilize engineered gas compositions (Hydrogen, Nitrogen, Argon, or Dissociated Ammonia) to maintain thermodynamic equilibrium, reduce surface oxides, and support high-volume continuous output.
Core Technical Advantages
- Active Chemical Surface Reduction: Purified hydrogen-rich streams strip oxide films from metallic powder compacts during heating.
- Continuous High-Volume Processing: Integrates directly with continuous manufacturing capabilities mesh belt and pusher furnace lines for maximum thermal efficiency.
- Precise Carbon Potential Control: Prevents unwanted surface decarburization in high-strength structural PM parts.
Target Material Categories
Technical Performance & Metric Comparison
Comprehensive operational evaluation to assist metallurgy and process engineering teams in specifying furnace architectures based on throughput, material chemistry, and target density.
| Performance Parameter | Vacuum Sintering Furnace | Controlled Atmosphere Sintering | Engineering Impact |
|---|---|---|---|
| Degassing Efficiency | Optimal (10-3 Pa base vacuum) | Moderate (Purge gas sweep dependent) | Vacuum vaporizes organic binders efficiently without trapping micro-voids or gas pockets. |
| Achievable Density | 98.0% – 99.8% Theoretical | 92.0% – 97.5% Theoretical | Vacuum consolidation achieves higher fatigue strength and hermetic sealing capability. |
| Operating Cost per kg | Higher (Batch cycle energy management) | Lower (Continuous high-throughput operations) | Controlled atmosphere furnaces deliver superior unit economics for high-volume production lines. |
| Thermal Field Uniformity | ±3°C to ±5°C (Multi-zone radiant heating) | ±5°C to ±8°C (Convective & radiant heat transfer) | Uniform vacuum hot zones eliminate atmospheric convection currents, ensuring consistent volumetric shrinkage. |
| Process Gas Consumption | Minimal (Partial-pressure gas dosing) | High (Continuous multi-zone purge volumes) | Atmosphere systems require dedicated gas supply lines, gas mixing units, and safety monitoring systems. |
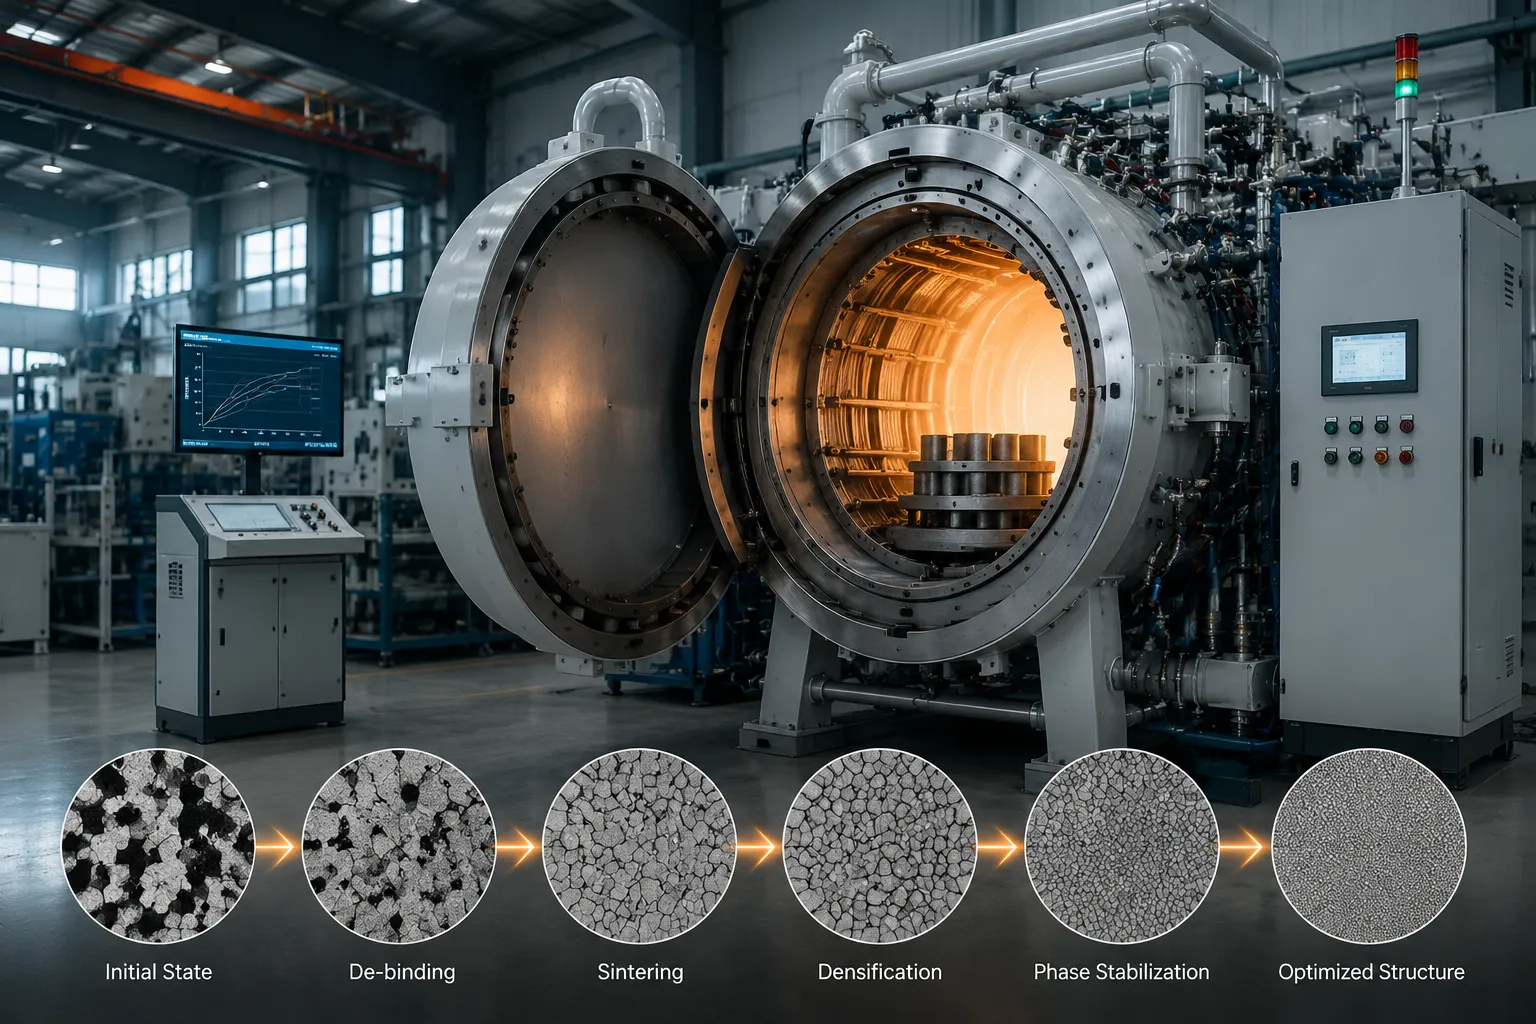
Optimizing Microstructural Densification and Phase Stability
Selecting the optimal media within a comprehensive sintering process guide requires balancing solid-state atomic diffusion with high-temperature chemical thermodynamics. In a high-temperature vacuum sintering furnace, operating under deep vacuum conditions (down to 10-3 Pa) prevents interstitial gas entrapment and oxidation in reactive metals like titanium, tantalum, and niobium. By removing ambient gas pressure during early ramp stages, volatile binders evacuate cleanly, enabling uninhibited pore closure and grain boundary migration to yield superior mechanical properties.
Conversely, controlled atmosphere sintering relies on active gas chemistry to influence metallurgical transformations during thermal processing. Incorporating high-purity hydrogen or nitrogen-hydrogen blends enables the chemical reduction of surface oxides on iron and copper powder metallurgy compacts. Precise dew-point monitoring and carbon potential regulation safeguard MIM stainless steel and tool steel components against surface decarburization, ensuring strict dimensional tolerances and predictable shrinkage rates across high-volume production cycles.
At Haitem Furnace, we engineer tailored vacuum and controlled atmosphere thermal processing equipment built around your specific alloy systems. Backed by our global service network and featuring multi-zone PID temperature control, automated gas mixing manifolds, and custom hot zone geometries, Haitem systems deliver tight thermal uniformity and repeatable processing performance for demanding global manufacturing environments.
Need assistance evaluating atmosphere requirements for your alloy?
Haitem Furnace offers material evaluation, thermal field simulations, and custom furnace engineering proposals tailored to your precise throughput and density requirements.
Material Specific Sintering Process Application Guide
Consolidating metallic powders and advanced ceramics into high-density components demands rigorous control over thermal profiles, atmosphere chemistries, and shrinkage kinetics. Explore how specialized thermal processing configurations optimize material density, mechanical integrity, and dimensional tolerances across Powder Metallurgy, Metal Injection Molding, and Advanced Ceramics.
Powder Metallurgy Sintering
Engineered for press-and-sinter iron-based and copper-based structural parts requiring tight dimensional repeatability, controlled porosity, and high mechanical endurance under cyclic loading.
- Atomic Diffusion: Solid-state neck formation and pore rounding between metal grains.
- Carbon Control: Precise atmosphere dew-point tracking to prevent surface decarburization.
- Application Focus: Automotive transmission gears, oil pump rotors, and timing sprockets.
MIM Sintering Process
Tailored for complex, high-binder-content components requiring thorough binder removal, high linear shrinkage control, and exceptional final theoretical density.
- Thermal Debinding: Complete outgassing of organic backbones without shape distortion.
- High Densification: Rapid pore closure achieving hermetic-grade stainless steel parts.
- Application Focus: Surgical instruments, firearm components, and consumer electronics hardware.
Advanced Ceramics Sintering
Formulated for extreme thermal environments requiring liquid-phase or solid-state consolidation of alumina, silicon nitride, and silicon carbide green bodies.
- Microstructure Engineering: Suppressing grain growth while driving full boundary migration.
- Decomposition Control: Overpressure nitrogen environments preventing dissociation at >1750°C.
- Application Focus: Semiconductor wafer chucks, ballistic armor plates, and ceramic bearings.
Industrial Material Sintering Parameter Comparison Matrix
Technical baseline for thermal profile setup, gas atmosphere selection, and critical shrinkage expectations.
| Material Classification | Benchmark Grade | Peak Temperature | Atmosphere / Vacuum Level | Linear Shrinkage | Critical Process Parameter |
|---|---|---|---|---|---|
| Iron-Based PM | FC-0208 / FN-0205 | 1120°C – 1150°C | 90% N2 / 10% H2 (Dew Pt < -40°C) | 0.2% – 0.5% | Sinter-hardening rapid cooling rate control |
| Stainless Steel MIM | 316L / 17-4PH | 1340°C – 1380°C | High Vacuum (10⁻² Pa) or Pure H2 | 15% – 18% | Carbon content balance and chromium oxidation prevention |
| Titanium Alloy MIM | Ti-6Al-4V | 1250°C – 1320°C | Ultra-High Vacuum (10⁻³ Pa) | 14% – 17% | Strict interstitial oxygen pick-up suppression (<0.15%) |
| Nitride Ceramics | Silicon Nitride (Si3N4) | 1750°C – 1850°C | Overpressure Nitrogen (1.0 – 9.9 MPa) | 16% – 20% | Thermal decomposition suppression via positive N2 pressure |
| Carbide Ceramics | Sintered SiC (SSiC) | 1950°C – 2100°C | Argon Atmosphere / High Vacuum | 14% – 18% | Sub-micron grain boundary phase tailoring with B/C additives |
Optimizing Process Windows for Next-Generation Materials
Successful consolidation depends on maintaining exact thermal gradients across every stage of the heat treatment cycle. Whether processing high-volume powder metallurgy structural gears or high-purity ceramic green bodies, Haitem Furnace integrates multi-zone PID thermal control with precise atmosphere management to eliminate thermal stresses and guarantee batch-to-batch repeatability across every industry we serve.
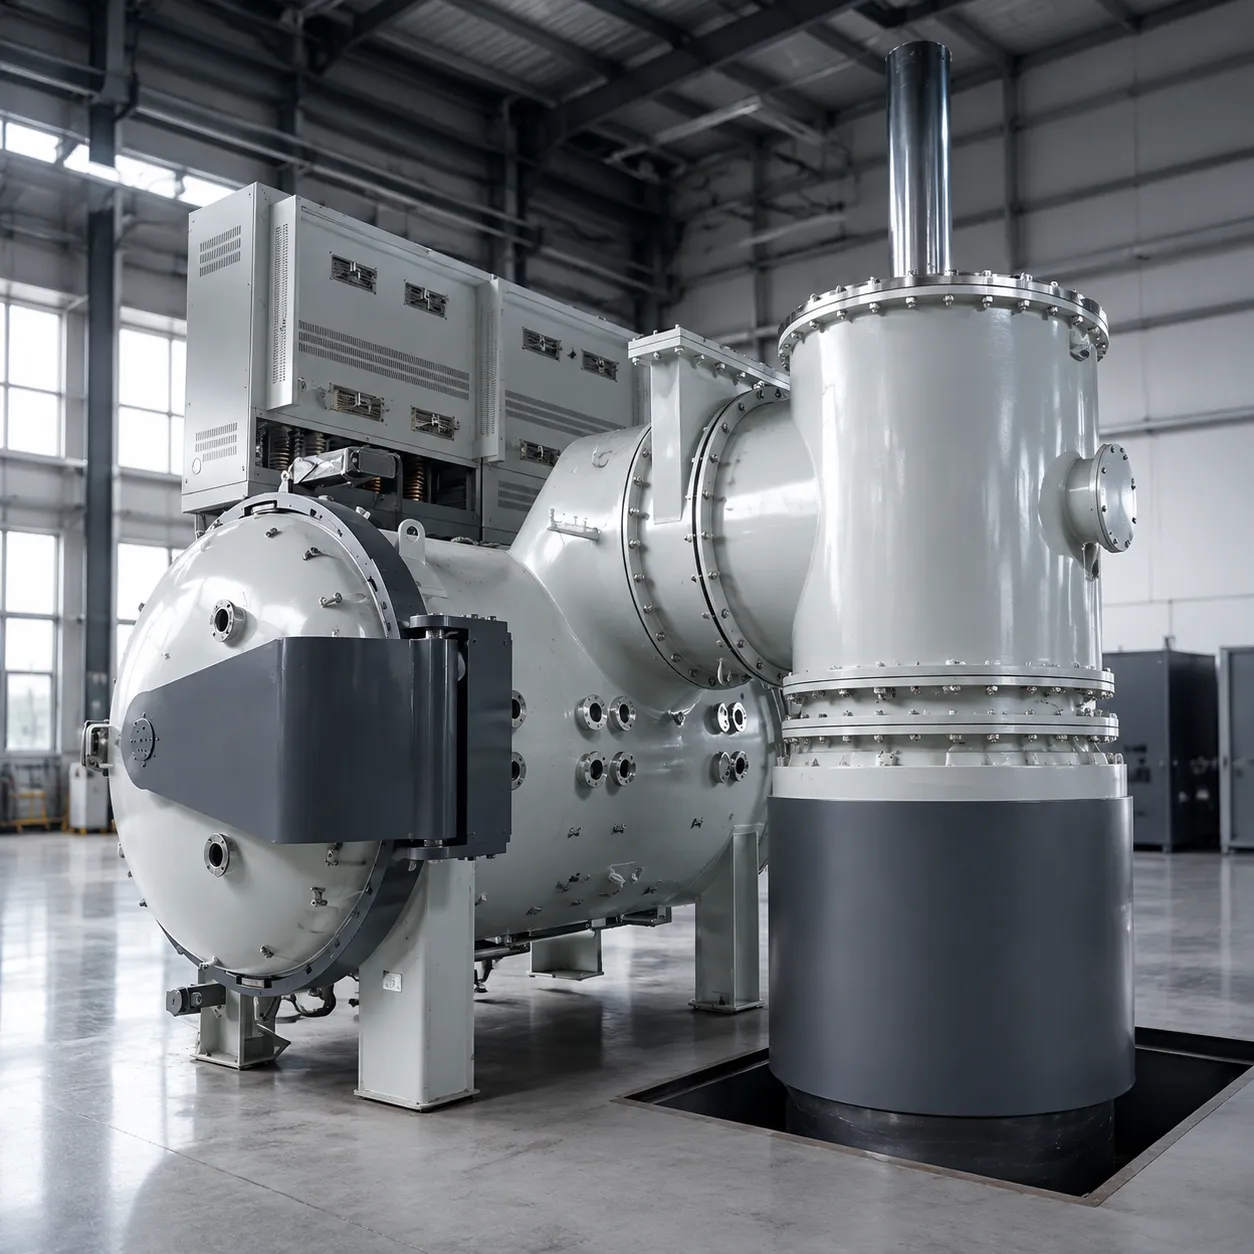
Powder Metallurgy Sintering Dynamics and Mass Production
In industrial powder metallurgy sintering, mechanical integrity relies on atomic transport mechanisms across contact points between pressed metal grains. As green compacts pass through the heating zones, thermal energy initiates solid-state diffusion, forming interparticle necks that eliminate pore spaces and dramatically increase tensile strength.
Controlling the sintering atmosphere is vital when processing iron-carbon or copper-steel alloys. Utilizing endothermic gas or high-purity nitrogen-hydrogen gas mixtures maintains a protective shield that prevents oxidation and controls surface carbon content. Haitem Furnace designs continuous mesh belt and pusher furnace systems engineered with controlled cooling zones, enabling in-line sinter-hardening to yield superior martensitic microstructures without secondary heat treatment.
Precision MIM Sintering Process and Volumetric Shrinkage Control
The MIM sintering process presents complex thermal dynamics due to the removal of high-fraction organic binder systems (typically 30% to 50% by volume). Thermal processing requires a distinct two-stage thermal lifecycle: thermal debinding under partial pressure or controlled flow to volatilize binder polymers, followed immediately by high-temperature densification up to 99.5% theoretical density.
Because MIM parts experience up to 22% linear shrinkage, thermal field non-uniformity of even a few degrees can cause severe warpage, sagging, or dimensional variance. For demanding alloys like MIM Stainless Steel 316L processed at 1360°C in pure hydrogen, or Ti-6Al-4V consolidated under high vacuum, Haitem’s vacuum debinding and sintering furnaces feature all-metal or graphite hot zones designed to maintain ±1°C uniformity, protecting part geometry and mechanical performance.
Ultra-High Temperature Advanced Ceramics Sintering
Advanced ceramics sintering requires extreme thermal capability. Structural ceramics such as Alumina (Al2O3), Silicon Nitride (Si3N4), and Silicon Carbide (SiC) demand processing temperatures ranging from 1500°C to well over 2400°C. At these extreme levels, pore boundary migration must be carefully synchronized with grain growth kinetics to achieve ultra-high density without coarsening microstructures.
When sintering covalent ceramics like silicon nitride, nitrogen overpressure sintering (GPS) is required to suppress high-temperature thermal decomposition. Haitem Furnace supplies specialized ultra-high temperature vacuum and gas pressure furnaces equipped with graphite heating elements and multi-layer thermal insulation, providing safe, high-purity processing environments for semiconductor, aerospace, and defense applications.
Experimental Validation and Process Development Support
Navigating exact sintering parameters for new powder formulations or complex geometric green bodies requires empirical testing. Haitem Furnace operates advanced thermal testing facilities to help engineering teams establish optimal ramp rates, soak times, and atmosphere ratios. Our technical team works alongside your engineers to perform atmosphere dew-point optimization, vacuum thermal profiling, and metallurgical sample evaluation before equipment design and commissioning.
Industrial Sintering Furnace Selection: Batch vs Continuous Systems
Evaluating furnace architecture is critical to optimizing thermal processing performance and total cost of ownership. Haitem Furnace delivers engineered sintering solutions spanning flexible batch vacuum systems to fully automated continuous production lines, ensuring your equipment directly matches production volume, metallurgical standards, and operational workflows.
Match Equipment Architecture to Your Target Capacity
Selecting between a batch vacuum system and a continuous sintering furnace requires balancing component complexity against daily throughput goals. Aligning thermal ramp cycles, atmosphere purity, and mechanical conveyance with your target output minimizes per-part energy consumption and prevents line bottlenecks. To explore our complete product catalog and system specifications, consult our engineering team.
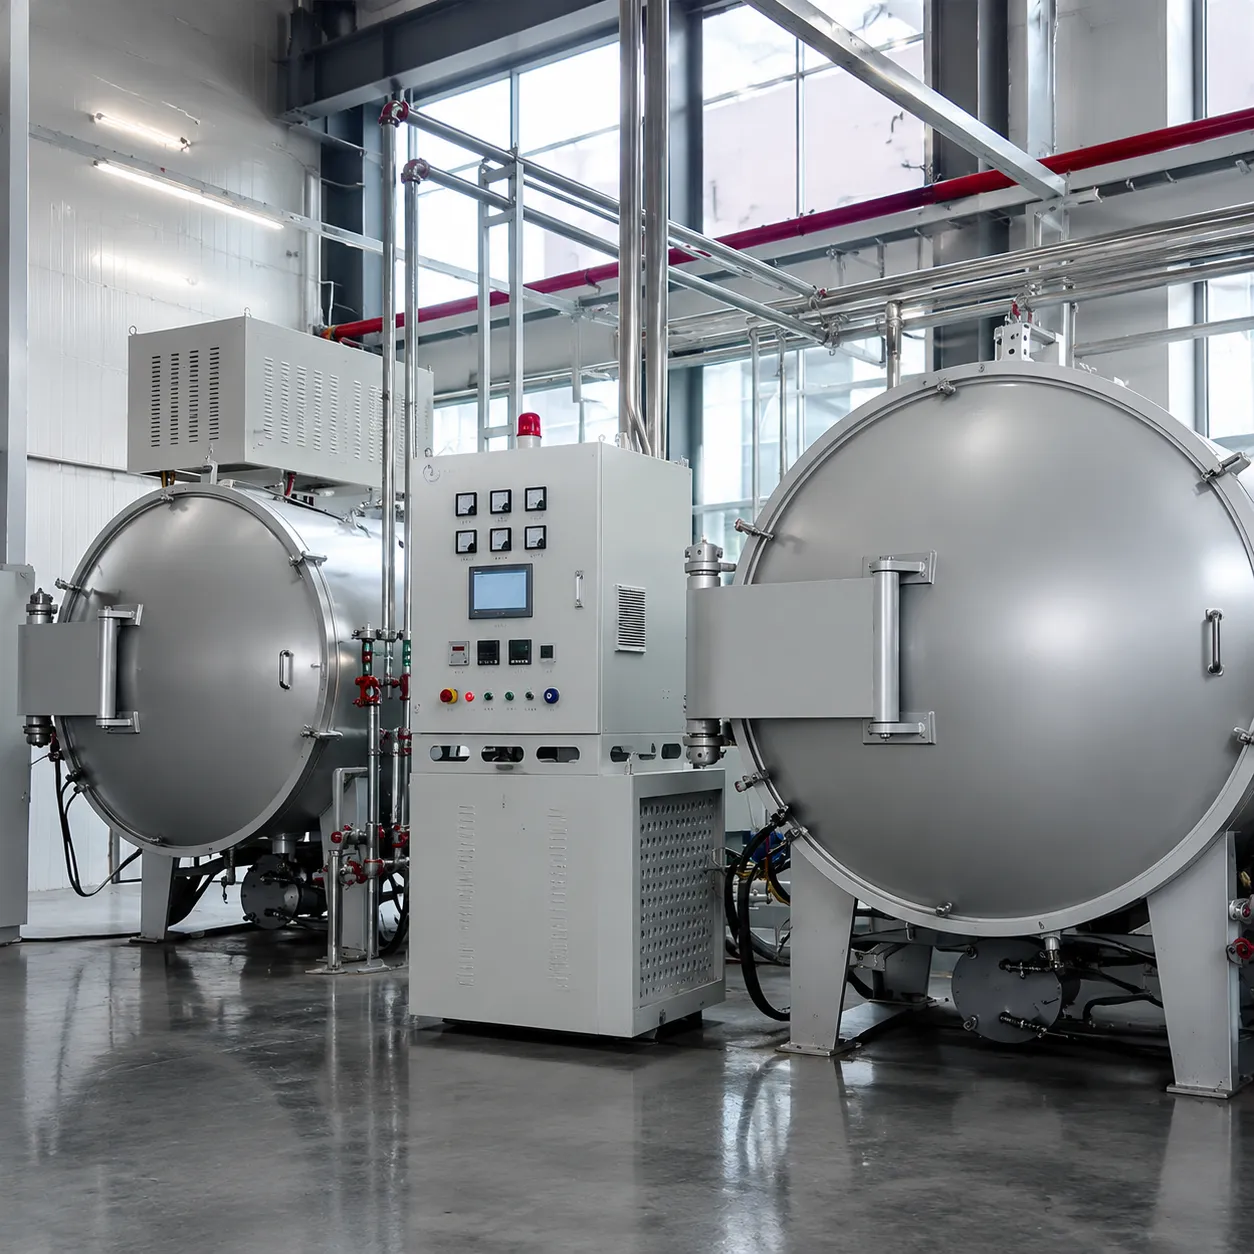
Batch Sintering Furnaces
Engineered for specialized metallurgy requiring tight atmosphere control, deep vacuum isolation, and highly adaptable thermal profiles. Batch systems allow engineering teams to execute distinct ramp, soak, and cooling schedules for every load.
Key Technical Advantages
- Deep Vacuum Isolation: Reaches vacuum levels down to 10⁻³ Pa with optional forced inert gas quenching for grain refinement.
- Multi-Stage Profile Control: Programmable PID control tailored for delicate debinding, pre-sintering, and high-temperature soaking.
- Target Applications: High-mix/low-volume production, aerospace components, medical implants, and advanced R&D.
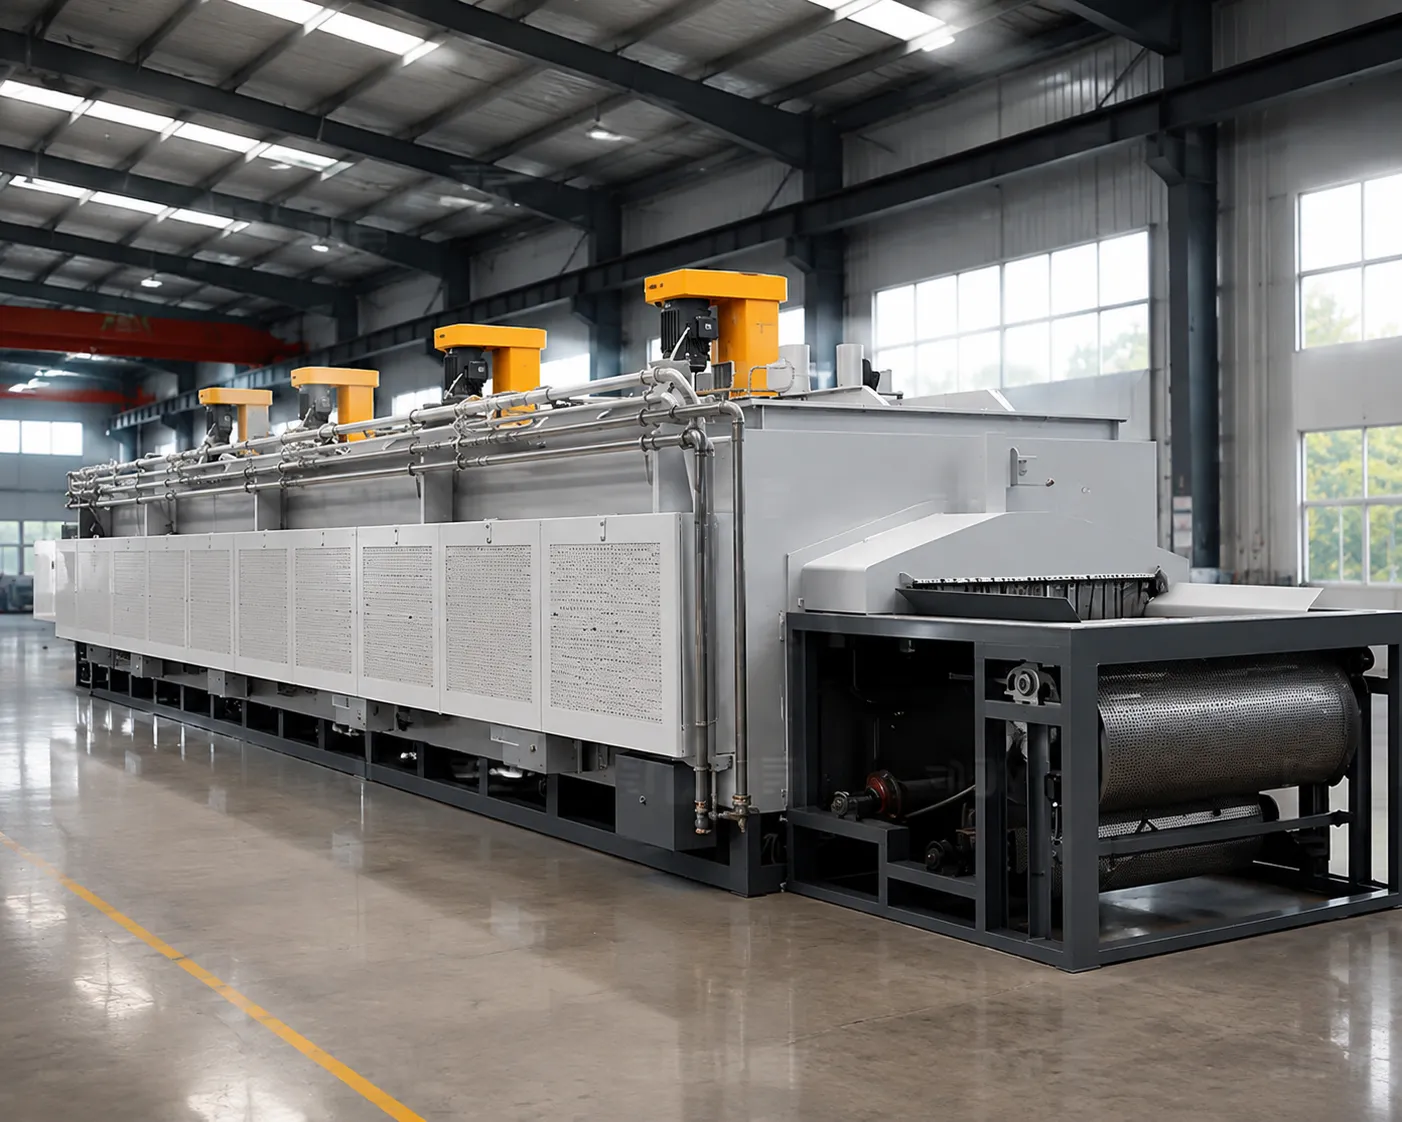
Continuous Sintering Furnaces
Built for continuous thermal processing using automated mesh belt, pusher, or roller hearth conveyance. Continuous systems maintain steady-state temperature zones and controlled gas flow for uninterrupted high-volume manufacturing leveraging our advanced manufacturing-capabilities.
Key Technical Advantages
- Automated Conveyance Options: Heavy-duty mesh belt, hydraulic pusher, or precision roller hearth drives engineered for continuous operation.
- Zoned Atmosphere Management: Multizone gas injection preserves continuous protective gas curtaining and low dew-point integrity.
- Target Applications: Mass-market powder metallurgy (PM), MIM automotive parts, structural components, and high-volume hardware.
Architecture Decision Matrix
Side-by-side engineering evaluation guide for plant operations and procurement teams.
| Performance Category | Batch Vacuum Furnaces | Continuous Conveyor Systems |
|---|---|---|
| Production Profile | High-Mix / Low-to-Medium Output | Standardized Mass Production |
| Atmosphere & Vacuum | Ultra-High Vacuum (10⁻³ Pa) & Inert Gas | Continuous Protective Gas Curtain (H₂/N₂/Ar) |
| Thermal Profile Flexibility | Fully Variable Cycle per Individual Batch | Fixed Steady-State Temperature Zones |
| Energy & Utility Overhead | Cyclic Thermal Load per Batch Run | Low Per-Unit Overhead via Continuous Operation |
| Typical Industry Fit | Aerospace, Medical, Refractory Metals, R&D | Automotive PM Parts, MIM Components, Hardware |
Sintering Defects Troubleshooting & Precision Temperature Control
Achieving high-density consolidation and tight dimensional tolerances in thermal processing demands absolute thermal field control and active atmosphere management. When structural defects such as micro-cracking, oxidation, or asymmetric shrinkage threaten production yields, systematic root-cause diagnostics are critical. Explore technical troubleshooting protocols developed by engineers at Haitem Furnace to isolate failures, fine-tune temperature profiles, and optimize furnace performance. Learn more about-us and how client trust underpins our technical support.
Q1 What causes micro-cracking or fracturing in sintered parts, and how can it be resolved?
Micro-cracking and structural fracturing during sintering typically stem from three primary root causes in the thermal lifecycle: excessive heating ramp rates, steep thermal gradients across setter plates, or unmanaged debinding gas evolution. During debinding and presintering between 200°C and 600°C, organic binders decompose rapidly. If thermal ramping is too steep or carrier gas evacuation is insufficient, internal pore gas pressure quickly exceeds the green body's ultimate tensile strength, causing internal delamination and surface micro-fissures.
Actionable Diagnostic Protocol
- Optimize Debinding Ramp Rates: Lower thermal ramp speeds to 0.5°C–1.5°C per minute through the binder burnout zone inside a dedicated debinding furnace or pre-heating region.
- Balance Thermal Gradient Uniformity: Recalibrate multi-zone PID heating elements and refractory insulation to maintain thermal field variations strictly within ±1°C across the entire load area.
- Enhance Atmosphere Sweep Velocity: Increase protective carrier gas velocity (such as high-purity N2 or Ar) to continuously flush degraded polymer gas byproducts out of the hot zone before redeposition occurs.
Q2 How can sample oxidation and surface discoloration be eliminated during sintering?
Surface oxidation, scaling, and discoloration indicate elevated partial pressures of oxygen or moisture inside the hot zone at high temperatures. Common vulnerabilities include degraded elastomer door seals, micro-leaks in water-cooling jackets, contaminated process gas supply lines, or insufficient vacuum levels in controlled atmosphere sintering setups.
Preventative Operational Measures
- Integrate In-Line Dew-Point & Oxygen Monitoring: Continuously monitor protective gas lines, maintaining inlet gas dew points below -60°C and oxygen contamination under 5 ppm.
- Conduct Helium Mass Spectrometer Leak Detection: Inspect chamber sealing integrity and dynamic flange seals to verify ultimate vacuum levels reach 10-3 Pa prior to thermal ramp-up.
- Utilize Active Reducing Atmospheres: Introduce controlled hydrogen (H2) or dissociated ammonia gas blends to actively reduce residual surface metal oxides during high-temperature dwell cycles.
Q3 How do you correct non-uniform volumetric shrinkage or dimensional variance?
Inconsistent volumetric shrinkage and geometry distortion in Metal Injection Molding (MIM) or powder metallurgy components usually originate from radiant heat asymmetry inside the chamber, mechanical drag along setter plates, or uneven green body packing density established during compaction.
Process Alignment Solutions
- Optimize Heating Element Configuration: Re-balance multi-zone heating element geometry to eliminate cold corners and achieve isotropic radiant heat distribution.
- Upgrade High-Purity Ceramic Setter Plates: Transition to low-friction alumina, zirconia, or graphite setters coated with inert washes to permit unhindered lateral shrinkage.
- Standardize Powder Compaction Density: Audit green body density distributions using precision dimensional gauging and automated compaction control to prevent localized density gradients.
Q4 What causes internal porosity and inadequate final density in technical ceramics and metals?
Incomplete pore elimination during advanced ceramics sintering or alloy consolidation indicates insufficient peak temperature dwell, inadequate vacuum outgassing, or uninhibited grain boundary growth that traps pore voids inside grains before solid-state diffusion can close them.
Density Optimization Protocol
- Extend Peak Operating Temperature Dwell: Calibrate holding duration at peak temperatures (up to 2400°C) to promote atomic diffusion pathways and full pore elimination.
- Maintain High Vacuum Levels: Sustain high vacuum conditions (10-3 Pa or higher) in advanced vacuum furnaces to continuously pull trapped gas out of closing pore networks.
- Incorporate Grain Growth Inhibitors: Utilize dopants and controlled cooling schedules to stabilize grain boundaries and prevent premature pore trapping during densification.
Lab-Grade Defect Evaluation
Struggling with microstructural anomalies or unexplained batch distortion? Haitem Furnace provides complete metallurgical diagnostic services, hot-zone thermal field profiling, and process optimization support.
Sintering Defect Diagnostic Reference Matrix
Quick diagnostic lookup matching material failure modes to precise thermal control solutions.
| Observed Defect Mode | Primary Physical Cause | Target Parameter Control | Haitem Furnace Equipment Solution |
|---|---|---|---|
| Surface Blistering & Cracking | Rapid binder volatilization and internal gas expansion | Debinding ramp ≤ 1°C/min (200°C–600°C) | Multi-stage programmable PID thermal controller & vacuum debinding system |
| Oxidation & Decarburization | Moisture or trace oxygen ingress in process gas stream | Dew point ≤ -60°C; O2 < 5 ppm | High-purity atmosphere gas panel & hermetic chamber seal architecture |
| Warping & Distortion | Asymmetric heat radiation or setter plate friction drag | Thermal field variation ±1°C | Multi-zone heating element geometry & ceramic setter plates |
| Inadequate Hardness & Low Density | Residual micro-porosity and premature grain boundary growth | Vacuum levels reaching 10-3 Pa | High-vacuum molybdenum/graphite hot-zone furnace architecture |
Resolve Sintering Quality Issues with Haitem Furnace Experts
Send your defective sample specifications or heating profiles to our thermal process engineers. We provide comprehensive root-cause failure evaluations and recommend optimized hot-zone hardware tailored to your exact manufacturing requirements.
Ready to Elevate Your Sintering Quality and Production Yield?
Partner with Haitem Furnace to engineer high-performance industrial sintering systems tailored to your exact material requirements and operating specs. Learn more about us and our specialized solutions.
Material & Process Assessments
Comprehensive testing to evaluate densification, grain boundary kinetics, and atmosphere interactions backed by our advanced manufacturing capabilities.
Thermal Field & CFD Modeling
Advanced CFD airflow and heat distribution modeling to ensure strict thermal uniformity across load zones.
Tailored Equipment Proposals
Turnkey furnace designs including high-performance vacuum furnaces featuring precise temperature profiling, controlled atmospheres, and automation options.
WhatsApp Engineering Support
+86 180 1288 4174Technical Support Email
info@haitemfurnace.comRequest Technical Consultation
Submit your operating parameters to receive a customized equipment and process proposal.
Precision Industrial Systems Engineered to ISO 9001 Standards
Haitem Furnace delivers custom thermal processing engineering worldwide.